Allied Pumps supplies custom-built fire protection systems for commercial, residential, and public infrastructure.
Plan Your Fire Protection Needs
Our team has years of experience helping clients find the right fire protection solution for their project. Get in touch to find out more about our products and compliance with Australian Standards.
OVERVIEW
Fire Protection Systems Tailored to Your Site
Allied Pumps designs and supplies complete fire protection systems for commercial, residential, and public infrastructure projects across Australia.
Our solutions are engineered to provide reliable fire water delivery, helping protect people, property, and critical assets. From fire tanks to fully integrated pump solutions, we deliver fire protection systems tailored to the specific requirements of each project.
SOLUTIONS
Our Fire Protection Solutions
Commercial Buildings
Helping safeguard offices, warehouses, retail centres, and industrial facilities.
Precision-engineered fire pumps designed to deliver reliable pressure and dependable protection across demanding commercial and infrastructure projects.
Allied Pumps delivers complete fire protection systems tailored to the specific requirements of each project. From initial consultation and engineering through to manufacturing commissioning, every stage is managed to ensure reliable fire protection.
Consultation & Design
We work with you to develop a fire protection system that meets your requirements.
Manufacturing
All fire protection systems are manufactured in-house at out our Canning Vale facility.
Delivery, Installation & Support
Your fire protection system is delivered to site with technical support and relevant documentation.
PROJECTS
Our Fire Protection Projects
Explore our case studies highlighting recently fire protection projects in the commercial, residential, and public sectors.
Due to the hot weather that is common throughout the year in the Pilbara region, water stored in potable water tanks can often reach temperatures in excess of 40 degrees. This is unacceptable for applications such drinking and eye wash stations and we needed to come up with a solution to accommodate this. We also provided the fire protection for a new Sino Iron Steel Warehouse in a tight 6 week deadline. Keep an eye out for the Fire Protection provided and find out more about the Eye Wash Station below.
Canal Rocks Beachfront Resort sits waterfront at Smiths Beach in Yallingup. It offers beautiful accommodation for families, friends and couples visiting Yallingup and its surroundings. The facility required a fire pro pump set. We used the first AS2941-2013, which we designed, manufactured and installed the system, ensuring it met all standards and regulations. The project had its challenges since it was a first, however its successful completion enabled us to learn valuable information which will help in future installations. The project highlighted our ability to quickly learn on the job whilst successfully completing the project brief.
The Roy Hill railway is a 344km standard gauge, single line, heavy haul railway built to transport 55Mtpa of iron ore from the Roy Hill Mine to the Port stockyard facility, in the Boodarie Industrial Estate south of Port Hedland. This operation uses a lot of diesel and was in need of a large bulk diesel facility to rapidly fuel the trains to meet production and delivery demands. This would allow them to function more efficiently. Nothing of this nature had ever been accomplished. Traditionally fuel facilities have pumps for unloading, loading and other refuelling activities located around the site and are wired back to a Motor Control Centre building. Our solution was to consolidate the pumping, compressed air equipment and Motor Control Centre onto a single super skid. The skid was pre-fabricated, assembled and tested at our facility and lifted into place on site where only a single lift was required. The project was delivered on time and as requested.
Mundella was looking to reinvent an industrial filling system and outdated production line. The brief was to provide a food grade, fully compliant solution for the careful transfer of yoghurts and dairy products from vats, while maintaining constant and sensitive flow rates and meeting specific hygiene requirements. We engineered and manufactured an innovative solution to an outdated processing line using a mobile Wilden pumping package. Read on to find out how we achieved this.
Allied Pumps has a long history with Busselton, and in particular the famous Busselton Jetty. In 2000 we supplied a sewage pump station – designed to hang underneath the jetty under the centre. 18 years later the system is still in good condition and is testament to the high quality product working as hard today as it was when it was installed. In addition to this sewage pump station, we also supplied a concrete pump station and sewage pump station at the Underwater Observatory. More recently we supplied pump stations for the on-shore discovery centre.
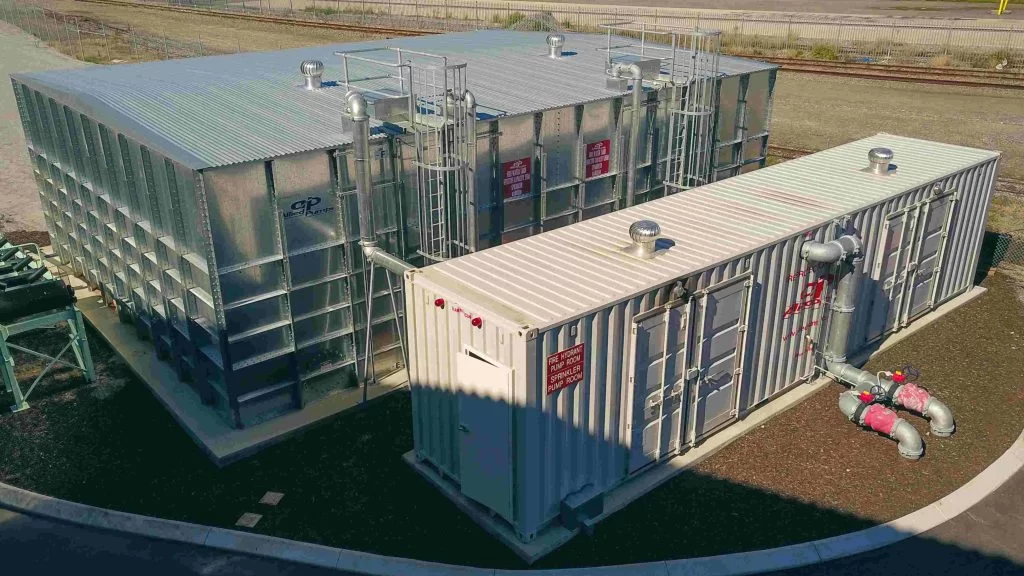
The Craft Street project involved 8 adjoining lots which required fire protection. To solve this problem, two (2) tanks measuring 5.12 m in diameter by 9.20 m high were assembled onsite and situated next to a fire pumpset in its own custom built enclosure. By collaborating, the owners of the 8 lots were able to share the costs and find a collective solution that worked for them. The short lead time was met and we were able to meet the client expectations in the provided timeframe.
It’s been 25 years, and the Bickley Booster Pump Station is still going strong. In 1992, we took on this project. This challenge began with the need to solve a low-pressure problem in the Orange Grove area. A dual pump system operating on a variable speed control was installed. This included the base, pipework, valves, control system and pressure vessel. The pump set is still functioning correctly and addressing the original issue. This project represents the quality and endurance of our pump systems.
Allied Pumps creates insulated circular steel panel liner tank for the Karratha Health Campus to meet clients cold water requirements. We were able to meet the client’s stringent requirements to produce a cost effective, potable water tank that could withstand the extreme weather conditions. Rising to the challenge, this project was Allied Pumps first insulated circular steel panel liner tank complete with a cold water circulating program.
Formed in 1905 to obtain, treat and distribute water supplies, the Bunbury Water Board has served the people of Bunbury for over 100 years. The city’s early settlers knew of water stored naturally underground and tried to use it to replace the Collie River and the Preston River, which were the only sources of water for drinking in those days. We supplied the first variable speed system to the water authority. It’s still being used today.
Allied Pumps recently provided 2 Circular Colour Finished Steel Water Storage Tanks to a client near the edge of the water at the Kwinana Bulk Jetty. This area of Cockburn Sound is of significant economic and social importance as it facilitates trade to Western Australia and the nation. It is also subjected to very high winds (almost cyclonic during bad weather events) so special design considerations had to be incorporated into the tank design and construction. The tanks were constructed to 3mm in thickness all over (instead of the normal 3mm on the bottom strake and 1.95mm on the others). The tanks were fitted with harness points on the roof and installed with 2 SWAH doors per tank (normally one). The tanks were also powder coated in colorbond Off White finish to fit in with the surroundings.
Allied Pumps delivered a custom fire water tank for a new shopping centre in Alkimos, WA, overcoming tight plant room constraints. The 90 kL, 6 m‑high rectangular steel panel liner tank met safety codes and provided compliant water storage where space was limited
Allied Pumps supplies complete fire protection systems, including fire pumps, fire water tanks, fire pump controllers, fire pump enclosures, sprinkler systems, hydrant systems, and containerised fire pump packages.
Yes, Allied Pumps manufactures fire water storage tanks in accordance with AS2304. Our tanks can also be integrated with fire pumps and controls as part of a complete solution.
Yes, Allied Pumps designs and manufactures fire pump enclosures to protect equipment from weather, dust, and harsh operating environments while providing easy access for maintenance.