Allied Pumps concrete pump stations are developed for multi-dwelling residential and commercial installations. They are commonly used in effluent schemes where twin pumps or larger storage volumes are required.
Precast concrete pits are moulded with a smooth, hard, impervious finish. These are designed for superior service life by combining high-strength 50 MPa concrete with sulphate resistant cement. Options for internal coatings, calcareous aggregate, or linings are also available.
Additionally, our concrete pump stations can be supplied with internal valve chambers fully sealed against the ingress of liquid or gas. This helps improve safety, serviceability, and long-term reliability.

This project was the result of a need to facilitate communication between two pump stations. One was located at Denmark High School; the other at Riverside Club. This project included supply, installation, and commission of control equipment. The objective was to pause the operation of the Riverside Club pump station when one of the pumps at the high school was operating. A dialler system was used to sync these two locations. We delivered the solution to connect these two systems which increased the efficiencies of the solutions.

Located on the Burswood Peninsula, the Optus Stadium is part of a large redevelopment that has become a draw card to thousands of people. However, as with all new developments there was a significant change to the existing landscape. Part of the Optus Stadium is bounded by the Swan River and river traffic, some of the retaining walls and steel piles on the water’s edge which could be seen from the water and needed to be addressed which could not be achieved using a land based planting scheme or additional construction. Allied Pumps created an environmentally sound and sustainable floating treatment wetland that can be configured in rafts of endless configurations. They can fit any existing space or water body shape and can operate in fluctuating water levels which was an essential requirement for this project. While the floating treatment wetlands are primarily a water treatment tool, they have the added bonus of being visually appealing with the use of wetland sedges, rushes and grasses providing fast and easy to install beautification options.

The Perth City Link bus port is reconnecting Northbridge with the city centre, extending from the Perth Station to the new Perth Arena. The bus port required sufficient water storage for protection against fire. Delivering water storage in an underground situation is challenging but necessary. We had several hurdles to overcome. Our ultimate solution was to recommend our dual diesel fire protection pump set. This included suction and discharge manifolds combined with dual rectangular steel liner panel tanks. We manufactured the complete fire pumps skid at our production facility, so they could be tested at our test facility. Installing the tanks onsite was then a challenge in the tight confines of the underground plant room. The successful outcome offered a sufficient amount of water that could be dumped quickly in the case of a sudden fire.

Station street markets were historic markets located in Subiaco that closed in 2015 after 30 years. In 2017, the site became part of a $96M redevelopment plan. We are currently working on this project constructing custom 4.70 diameter by 9.20 high fire water tanks (holding 150 kL each). These are custom specifications to meet the site’s needs. Creating custom length panels highlights our ingenuity and abilities to accommodate clients.

Eastern Goldfields Regional Prison is an Australian prison located in Boulder, Western Australia, and opened in 1980. An upgrade to the fire pump skid and commissioning was necessary in 2014. The primary challenge was carrying out both tasks at the same time including upgrading and commissioning. We worked hard to balance both tasks resulting in a successful delivery of the project.

The Roy Hill railway is a 344km standard gauge, single line, heavy haul railway built to transport 55Mtpa of iron ore from the Roy Hill Mine to the Port stockyard facility, in the Boodarie Industrial Estate south of Port Hedland. This operation uses a lot of diesel and was in need of a large bulk diesel facility to rapidly fuel the trains to meet production and delivery demands. This would allow them to function more efficiently. Nothing of this nature had ever been accomplished. Traditionally fuel facilities have pumps for unloading, loading and other refuelling activities located around the site and are wired back to a Motor Control Centre building. Our solution was to consolidate the pumping, compressed air equipment and Motor Control Centre onto a single super skid. The skid was pre-fabricated, assembled and tested at our facility and lifted into place on site where only a single lift was required. The project was delivered on time and as requested.
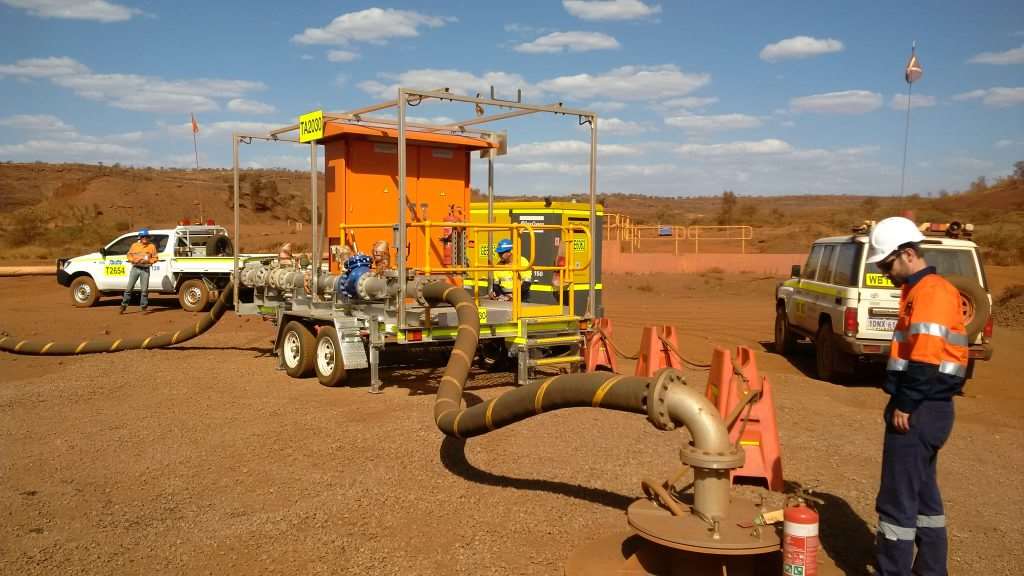
A below water table mine operation in the Shire of East Pilbara sustains the Newman Hub mining operations at a Western Australian iron ore mine site. The client needed an in-pit dewatering solution to discharge excess groundwater for a new section of the pit. The solution was required within eight weeks. A bore system using equipment that would suit their requirements was designed. We provided Kwikbore bore head works systems which were trailer-mounted. This would minimise dewatering and pumping downtime during removal of the existing equipment from the mining pit during blasting and installed the head works once the blasting was completed. Overall, six mobile head works systems were used, each featuring a unique plug and play design with remote telemetry system for integration with the site SCADA system. Our experienced technicians carried out onsite commissioning to effectively integrate the pumping systems into the BHP site-wide SCADA system. The project was delivered on time and on budget and operates to the specification set out in the scope of works.

This job represented a challenge as the insurance company who are the insurers of the BUNGE Grain Terminal required that a pumpset built to a North American standard be used on the job, otherwise they would not grant insurance cover. Insurance cover was conditional upon compliance with a standard for the fire pump not commonly used in Australia. This meant that a fire pump had to be specially imported from North America to supply to the fire company fitting out the fire services on site. Allied Pumps were able to work with an overseas Supplier to arrange the build and testing of the fire pump off shore, in a factory in North America, then arrange airfreight of some very heavy packages at considerable cost in order to reduce time lost in transit, to minimise delays in the building construction deadline. A further challenge was that there is NO LOCAL BACK UP for the North American controllers. Allied Pumps was able to rise to the occasion and overcome this challenge by our highly experienced technicians making contact with an overseas electrical technician to gain the knowledge necessary to overcome certain control panel commissioning obstacles. A fine outcome on a very challenging job!

Royal Perth Hospital is a 450-bed teaching hospital located on the north-eastern edge of the CBD of Perth in Western Australia. The project started with a site visit by us. We measured and discussed the design needs for the fire pump set refurbishment. The first step was to disable and remove the existing system. This removal was the same day as the new system’s delivery so there was no site storage required. The new system was then installed in one day. This was a quick turnaround time, and we were able to meet the timeframe to ensure minimal downtime.

The Cockburn Central Police Station required several tank and pump solutions. Initially a galvanised regular tank was recommended. However, there were design issues with the concrete slab. The station requested an in-situ concrete tank liner. The design was changed to meet this need. Allied Pumps was able to provide a turnkey solution for our client on this project, saving the client from having to engage the services of several different sub-contractors to work on various aspects of the tank installation. This enable the client to place a single order with us for all the work on the tank and supply of the pumping systems, enabling him to focus on other aspects of the project. The final project consisted of a panel tank, circulating pump pack, hot water circulator, fire pump and tank liner pack. The result was a seamless integration between the pumps and the tanks, and reliable fire protection has been the overall outcome.
Concrete pump stations are used in multi-dwelling residential installations, commercial developments, and common effluent schemes where twin pumps or larger storage volumes are required.
Yes, Allied Pumps’ concrete pump stations can be supplied with internal valve chambers that are fully sealed against ingress of liquid or gas.
Yes, Allied Pumps’ precast concrete pump stations come with twin or single pump options depending on your project requirements.
Allied Pumps’ precast concrete pump stations are designed to conform to OH&S requirements and eliminate routine confined space entries, reducing operational and maintenance risks.
Allied Pumps’ precast concrete pits use high-strength 50 MPa concrete with sulphate resistant cement, with options for internal coatings, calcareous aggregate, or linings.
























































































