Allied Pumps designs and manufactures robust fire pumps and integrated fire protection systems built for integration with hydrant and sprinkler systems.
Designed to meet Australian Standard AS2941, each pumpset is assembled on a common fabricated base with manifolds, valves, and controls to deliver a fully automated system. Available in diesel or electric configurations, these units can be tailored to suit plant rooms, tight infrastructure spaces, or large sites.
With in-house fabrication, factory testing to AS2417, and integrated pump control panel technology, Allied Pumps delivers dependable fire protection infrastructure that ensures reliable pressure and fast response when it matters most.

A residential complex in Perth required an innovative way to pump water to reduce power consumption and improve sustainability. In many new buildings, there is a push to use a single basement tank with basement pumps pressuring all the way to the top of the apartment block. However, Allied Pumps had a better solution. A small pump and tank at the basement of the apartment block transfers water to the rooftop tanks at a low flow, keeping the rooftop tank full. A smaller, variable speed pump supplies the top few floors, whilst the levels below are fed by gravity. With a roof top tank full of water at all times, even during a power outage, the system can still supply the residents with water. Smaller pumps, simpler control logic, and reduced tank capacities all kept initial costs low and provided huge benefits for the complex.

The Craft Street project involved 8 adjoining lots which required fire protection. To solve this problem, two (2) tanks measuring 5.12 m in diameter by 9.20 m high were assembled onsite and situated next to a fire pumpset in its own custom built enclosure. By collaborating, the owners of the 8 lots were able to share the costs and find a collective solution that worked for them. The short lead time was met and we were able to meet the client expectations in the provided timeframe.

Due to the hot weather that is common throughout the year in the Pilbara region, water stored in potable water tanks can often reach temperatures in excess of 40 degrees. This is unacceptable for applications such drinking and eye wash stations and we needed to come up with a solution to accommodate this. We also provided the fire protection for a new Sino Iron Steel Warehouse in a tight 6 week deadline. Keep an eye out for the Fire Protection provided and find out more about the Eye Wash Station below.

We were recently involved in supplying fire protection for Perth Airport. View the video to see the testing DFES conducted at the facilities in March 2017.

It’s been 25 years, and the Bickley Booster Pump Station is still going strong. In 1992, we took on this project. This challenge began with the need to solve a low-pressure problem in the Orange Grove area. A dual pump system operating on a variable speed control was installed. This included the base, pipework, valves, control system and pressure vessel. The pump set is still functioning correctly and addressing the original issue. This project represents the quality and endurance of our pump systems.

Formed in 1905 to obtain, treat and distribute water supplies, the Bunbury Water Board has served the people of Bunbury for over 100 years. The city’s early settlers knew of water stored naturally underground and tried to use it to replace the Collie River and the Preston River, which were the only sources of water for drinking in those days. We supplied the first variable speed system to the water authority. It’s still being used today.
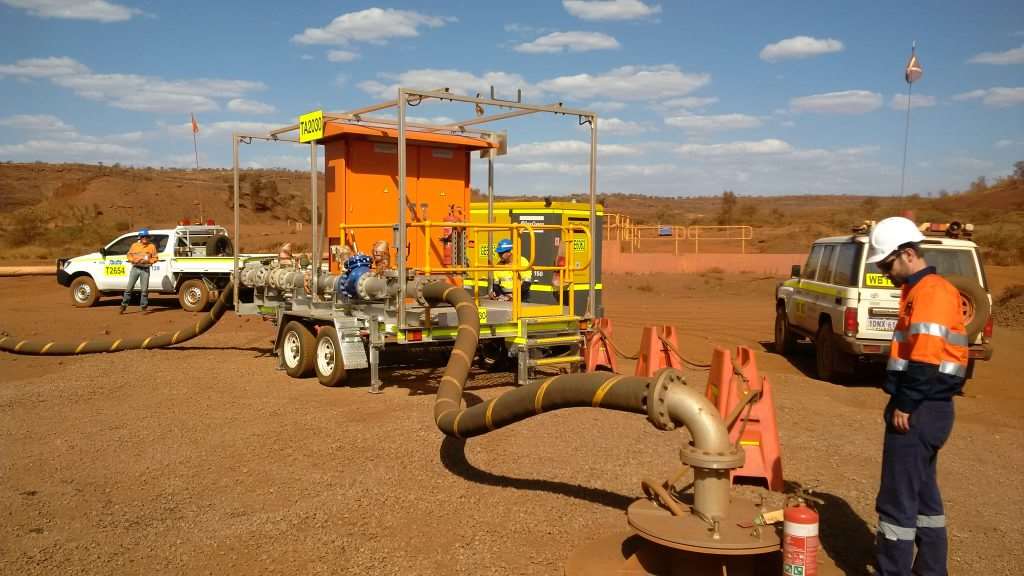
A below water table mine operation in the Shire of East Pilbara sustains the Newman Hub mining operations at a Western Australian iron ore mine site. The client needed an in-pit dewatering solution to discharge excess groundwater for a new section of the pit. The solution was required within eight weeks. A bore system using equipment that would suit their requirements was designed. We provided Kwikbore bore head works systems which were trailer-mounted. This would minimise dewatering and pumping downtime during removal of the existing equipment from the mining pit during blasting and installed the head works once the blasting was completed. Overall, six mobile head works systems were used, each featuring a unique plug and play design with remote telemetry system for integration with the site SCADA system. Our experienced technicians carried out onsite commissioning to effectively integrate the pumping systems into the BHP site-wide SCADA system. The project was delivered on time and on budget and operates to the specification set out in the scope of works.

The proposed fibreglass storage tank had an extended lead time of 14 weeks. To ensure schedules were kept, we recommended a galvanised tank, which was a first for us. This was an experience of trial and learning. Everything went smoothly providing the client with a viable solution within the requested timeframe.

Allied Pumps has a long history with Busselton, and in particular the famous Busselton Jetty. In 2000 we supplied a sewage pump station – designed to hang underneath the jetty under the centre. 18 years later the system is still in good condition and is testament to the high quality product working as hard today as it was when it was installed. In addition to this sewage pump station, we also supplied a concrete pump station and sewage pump station at the Underwater Observatory. More recently we supplied pump stations for the on-shore discovery centre.

Canal Rocks Beachfront Resort sits waterfront at Smiths Beach in Yallingup. It offers beautiful accommodation for families, friends and couples visiting Yallingup and its surroundings. The facility required a fire pro pump set. We used the first AS2941-2013, which we designed, manufactured and installed the system, ensuring it met all standards and regulations. The project had its challenges since it was a first, however its successful completion enabled us to learn valuable information which will help in future installations. The project highlighted our ability to quickly learn on the job whilst successfully completing the project brief.

Allied Pumps supplied a diesel/electric fire protection pumpset for an apartment fire in Cannington, proving its design under real emergency conditions. Built to strict Australian standards, the system worked exactly as intended, reaffirming that uncompromised safety and engineering matter when it counts.

Allied Pumps helped deliver a tailored fire protection solution for the underground Perth City Link Busport, redesigning pump and tank layouts to fit tight plant room constraints. The dual fire pumps and steel tanks provide sufficient water storage and protection for this critical transport hub.

Allied Pumps delivered a custom fire water tank for a new shopping centre in Alkimos, WA, overcoming tight plant room constraints. The 90 kL, 6 m‑high rectangular steel panel liner tank met safety codes and provided compliant water storage where space was limited.
Allied Pumps supplies diesel, electric, and diesel/electric fire pumps available in single, double or triple configurations.
Yes, Allied Pumps’ fire pumps are designed to be a complete package system and include all relevant valves, manifolds, and controls.
Yes, Allied Pumps’ fire pumps are designed in accordance with AS2941 and rigorously tested on our AS2417 in-house test rig.
Yes, Allied Pumps’ fire pumps come equipped with a Pyrokos fire pump controller.
Yes, Allied Pumps can supply weatherproof or sound-attenuated fire pump enclosures that provide easy maintenance access.
























































































