Allied Pumps designs and supplies jacking pumps (jockey pumps) that maintain pressure within fire protection systems during normal operation.
By automatically compensating for minor pressure losses caused by temperature changes or small system leaks, jacking pumps prevent the main fire pump from cycling unnecessarily.
This extends equipment life, improves system reliability, and ensures the fire protection system remains pressurised and ready to respond during an emergency.

Allied Pumps creates insulated circular steel panel liner tank for the Karratha Health Campus to meet clients cold water requirements. We were able to meet the client’s stringent requirements to produce a cost effective, potable water tank that could withstand the extreme weather conditions. Rising to the challenge, this project was Allied Pumps first insulated circular steel panel liner tank complete with a cold water circulating program.

Canal Rocks Beachfront Resort sits waterfront at Smiths Beach in Yallingup. It offers beautiful accommodation for families, friends and couples visiting Yallingup and its surroundings. The facility required a fire pro pump set. We used the first AS2941-2013, which we designed, manufactured and installed the system, ensuring it met all standards and regulations. The project had its challenges since it was a first, however its successful completion enabled us to learn valuable information which will help in future installations. The project highlighted our ability to quickly learn on the job whilst successfully completing the project brief.

Royal Perth Hospital is a 450-bed teaching hospital located on the north-eastern edge of the CBD of Perth in Western Australia. The project started with a site visit by us. We measured and discussed the design needs for the fire pump set refurbishment. The first step was to disable and remove the existing system. This removal was the same day as the new system’s delivery so there was no site storage required. The new system was then installed in one day. This was a quick turnaround time, and we were able to meet the timeframe to ensure minimal downtime.
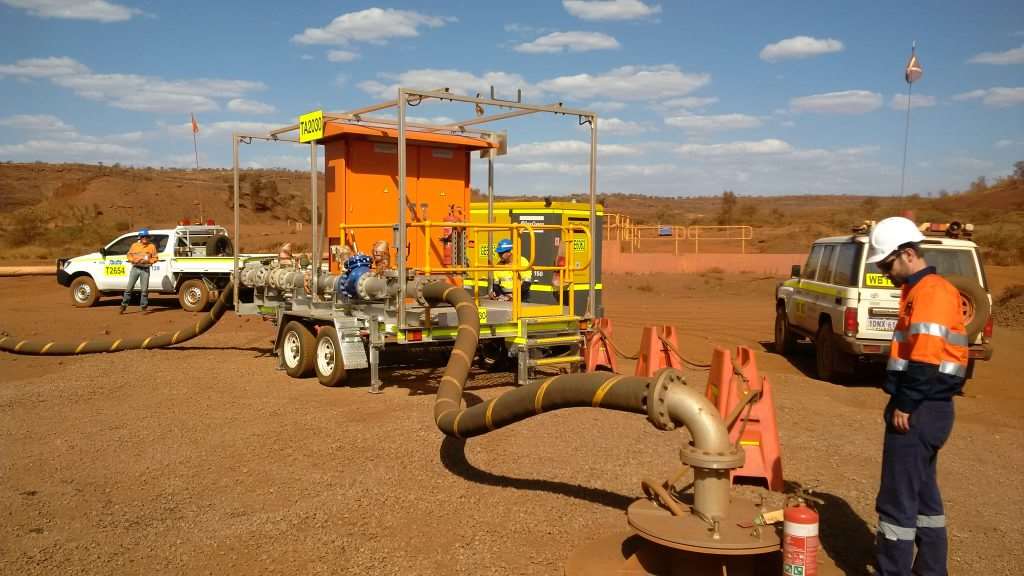
A below water table mine operation in the Shire of East Pilbara sustains the Newman Hub mining operations at a Western Australian iron ore mine site. The client needed an in-pit dewatering solution to discharge excess groundwater for a new section of the pit. The solution was required within eight weeks. A bore system using equipment that would suit their requirements was designed. We provided Kwikbore bore head works systems which were trailer-mounted. This would minimise dewatering and pumping downtime during removal of the existing equipment from the mining pit during blasting and installed the head works once the blasting was completed. Overall, six mobile head works systems were used, each featuring a unique plug and play design with remote telemetry system for integration with the site SCADA system. Our experienced technicians carried out onsite commissioning to effectively integrate the pumping systems into the BHP site-wide SCADA system. The project was delivered on time and on budget and operates to the specification set out in the scope of works.

The Australian Embassy in Jakarta, Indonesia required a water supply system. Because of its location, this was a very unique project. The spec required the materials to be stainless steel and fibreglass to resist corrosion. The site also needed a controller to monitor and operate water supply valves to fill tanks for use at the building. The three water supplies were the result of rainwater runoff from the roof, bore pumps and mains piping. To ensure that the specs were met, the valves were programmed to operate depending on the supply availability. The competing requirements of this project as well as working in a foreign environment created a number of challenges. We were able to rise to the challenge, through our strong organisational skills and execution of work.

Located on the Burswood Peninsula, the Optus Stadium is part of a large redevelopment that has become a draw card to thousands of people. However, as with all new developments there was a significant change to the existing landscape. Part of the Optus Stadium is bounded by the Swan River and river traffic, some of the retaining walls and steel piles on the water’s edge which could be seen from the water and needed to be addressed which could not be achieved using a land based planting scheme or additional construction. Allied Pumps created an environmentally sound and sustainable floating treatment wetland that can be configured in rafts of endless configurations. They can fit any existing space or water body shape and can operate in fluctuating water levels which was an essential requirement for this project. While the floating treatment wetlands are primarily a water treatment tool, they have the added bonus of being visually appealing with the use of wetland sedges, rushes and grasses providing fast and easy to install beautification options.

Mundella was looking to reinvent an industrial filling system and outdated production line. The brief was to provide a food grade, fully compliant solution for the careful transfer of yoghurts and dairy products from vats, while maintaining constant and sensitive flow rates and meeting specific hygiene requirements. We engineered and manufactured an innovative solution to an outdated processing line using a mobile Wilden pumping package. Read on to find out how we achieved this.

Allied Pumps rises to the challenge. Could we produce 20 relocatable bore head works, which could last for a minimum of 20 years and be compliant with wind loading requirements AS1170.2, for a wind region A4 quickly? Being headquarted in Western Australia, with extensive stock holdings, not only do we understand harsh conditions we were able to gear up quickly and meet the clients deadline.

Our client required new potable water and fire water storage tanks to be manufactured onsite. The location is particularly close to the harbour shoreline and situated in the category 5 cyclone region, which means winds can be in excess of 280 km per hr. This impacted every facet of design. We had extensive contact with suppliers to find alternative products that could withstand the aggressive environmental location. The process included a search for tank wall, nuts, and bolts all the way through to paints and roofing materials. We successfully installed all the equipment on schedule, within a 3 week period with no major disruptions or safety incidents. The tank construction was guaranteed for 25 years. The client was very satisfied with the end solution.

The Craft Street project involved 8 adjoining lots which required fire protection. To solve this problem, two (2) tanks measuring 5.12 m in diameter by 9.20 m high were assembled onsite and situated next to a fire pumpset in its own custom built enclosure. By collaborating, the owners of the 8 lots were able to share the costs and find a collective solution that worked for them. The short lead time was met and we were able to meet the client expectations in the provided timeframe.
A jacking pump automatically restores pressure lost through minor leaks or temperature fluctuations, preventing unnecessary operation of the main fire pump.
Yes, Allied Pumps supplies jacking pumps to integrate with complete systems composed of fire pumps, controllers, and associated equipment.
Yes, Allied Pumps supplies jacking pumps complete with dedicated Pyrokos fire controllers for automatic pressure maintenance.
Our jacking pumps are used in fire hydrant and fire sprinkler systems across commercial buildings, public infrastructure and high-rise developments.
Allied Pumps’ manufactures its jacking pump in Western Australia. Each system is assembled and tested in-house to ensure reliability and performance.
























































































