Muffin Monster grinders are a market-leading range of municipal wastewater shredders and screening systems. Their heavy-duty, precision-machined grinding systems are engineered for demanding wastewater and industrial treatment applications.
Available in channel and in-line configurations, the range includes compact grinders for limited-space installations, proven dual-shaft units for sewage and solids reduction, and powerful models for large sludge processing and industrial applications.
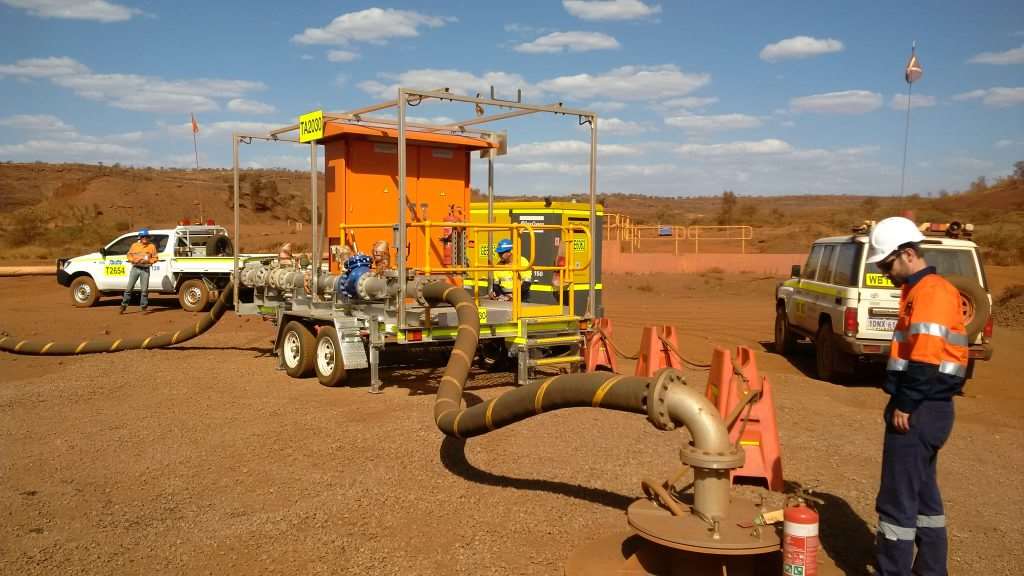
A below water table mine operation in the Shire of East Pilbara sustains the Newman Hub mining operations at a Western Australian iron ore mine site. The client needed an in-pit dewatering solution to discharge excess groundwater for a new section of the pit. The solution was required within eight weeks. A bore system using equipment that would suit their requirements was designed. We provided Kwikbore bore head works systems which were trailer-mounted. This would minimise dewatering and pumping downtime during removal of the existing equipment from the mining pit during blasting and installed the head works once the blasting was completed. Overall, six mobile head works systems were used, each featuring a unique plug and play design with remote telemetry system for integration with the site SCADA system. Our experienced technicians carried out onsite commissioning to effectively integrate the pumping systems into the BHP site-wide SCADA system. The project was delivered on time and on budget and operates to the specification set out in the scope of works.

The City of Subiaco had an initiative to improve water quality. The focus was on reducing pollutants in Lake Mabel Talbot. The lake is in the conservation category wetland under the Environment Protection policy and functions as a Water Corporation compensating basin. The lake collects rainfall runoff from four sub-catchments, totaling 300 ha. A Gross Pollutant Trap needed to treat the entire flow prior to entering the system, and our Baffle Box was the only system to appropriately meet the design criteria. The Baffle Box was able to catch leaves and other pollutants before they could enter the lake. The result of this project was cleaner water and an improvement in the water quality.

Royal Perth Hospital is a 450-bed teaching hospital located on the north-eastern edge of the CBD of Perth in Western Australia. The project started with a site visit by us. We measured and discussed the design needs for the fire pump set refurbishment. The first step was to disable and remove the existing system. This removal was the same day as the new system’s delivery so there was no site storage required. The new system was then installed in one day. This was a quick turnaround time, and we were able to meet the timeframe to ensure minimal downtime.

Located on Connelly Street at the Greater Sports Ground is the new built recreation & leisure centre incorporating the Kellerberrin & Districts Club. This was the site of the first concrete pump station in Western Australia. When wastewater has to get to the treatment facility and gravity is not cooperating, precast concrete pump stations do the heavy lifting. Precast concrete pump stations are designed, fabricated and installed with the highest-quality materials and equipment. We installed this system in the early 1990s. Completing a project like shows how we adopt innovation in out techniques.

The Craft Street project involved 8 adjoining lots which required fire protection. To solve this problem, two (2) tanks measuring 5.12 m in diameter by 9.20 m high were assembled onsite and situated next to a fire pumpset in its own custom built enclosure. By collaborating, the owners of the 8 lots were able to share the costs and find a collective solution that worked for them. The short lead time was met and we were able to meet the client expectations in the provided timeframe.

Allied Pumps creates insulated circular steel panel liner tank for the Karratha Health Campus to meet clients cold water requirements. We were able to meet the client’s stringent requirements to produce a cost effective, potable water tank that could withstand the extreme weather conditions. Rising to the challenge, this project was Allied Pumps first insulated circular steel panel liner tank complete with a cold water circulating program.

This project was the result of a need to facilitate communication between two pump stations. One was located at Denmark High School; the other at Riverside Club. This project included supply, installation, and commission of control equipment. The objective was to pause the operation of the Riverside Club pump station when one of the pumps at the high school was operating. A dialler system was used to sync these two locations. We delivered the solution to connect these two systems which increased the efficiencies of the solutions.

It’s been 25 years, and the Bickley Booster Pump Station is still going strong. In 1992, we took on this project. This challenge began with the need to solve a low-pressure problem in the Orange Grove area. A dual pump system operating on a variable speed control was installed. This included the base, pipework, valves, control system and pressure vessel. The pump set is still functioning correctly and addressing the original issue. This project represents the quality and endurance of our pump systems.

The Roy Hill railway is a 344km standard gauge, single line, heavy haul railway built to transport 55Mtpa of iron ore from the Roy Hill Mine to the Port stockyard facility, in the Boodarie Industrial Estate south of Port Hedland. This operation uses a lot of diesel and was in need of a large bulk diesel facility to rapidly fuel the trains to meet production and delivery demands. This would allow them to function more efficiently. Nothing of this nature had ever been accomplished. Traditionally fuel facilities have pumps for unloading, loading and other refuelling activities located around the site and are wired back to a Motor Control Centre building. Our solution was to consolidate the pumping, compressed air equipment and Motor Control Centre onto a single super skid. The skid was pre-fabricated, assembled and tested at our facility and lifted into place on site where only a single lift was required. The project was delivered on time and as requested.

Formed in 1905 to obtain, treat and distribute water supplies, the Bunbury Water Board has served the people of Bunbury for over 100 years. The city’s early settlers knew of water stored naturally underground and tried to use it to replace the Collie River and the Preston River, which were the only sources of water for drinking in those days. We supplied the first variable speed system to the water authority. It’s still being used today.
The 10K Series Muffin Monster is a compact grinder designed to fit into installations with limited space while still providing downstream equipment protection.
The 30K Series Muffin Monster uses a slow-speed, high-torque, dual-shaft design to shred tough solids that commonly cause sewer system problems.
The 40K Series Muffin Monster is designed for large sludge-processing systems and industrial applications such as food processing, petroleum, pulp and paper, chemical processing, and recycling.
Wipes Ready Technology is a two-dimensional cutting system that controls both the width and length of output material to reduce particle size and help prevent wipes from reweaving downstream.
Typical applications for the Muffin Monster grinders include sewage pumping stations, airports, sludge processing, headworks, grease receiving stations, marine waste, food waste, biogas facilities, and membrane bioreactors.
























































































