Allied Pumps supplies hydrant flow test kits that enable accurate testing of fire hydrant systems to verify flow rates, residual pressure, and overall system performance.
Designed for routine inspections, commissioning, and maintenance, our portable test kits provide a simple and reliable method of confirming hydrant system performance.
Pressure reading is obtained via a 0-1600 Kpa large face glycerine filled gauge. While flow readings are digital with instant and totalized flow readings displayed simultaneously.
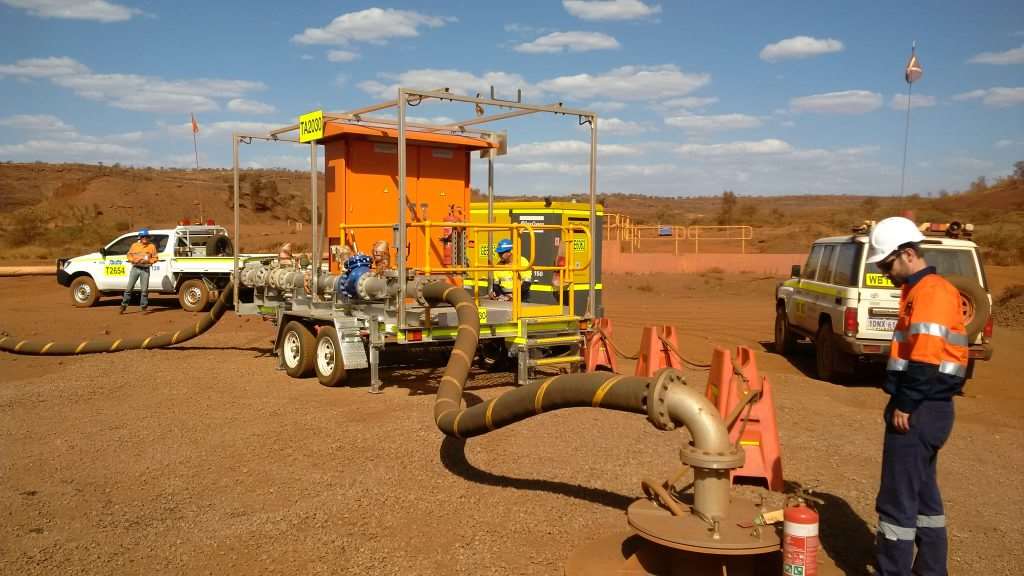
A below water table mine operation in the Shire of East Pilbara sustains the Newman Hub mining operations at a Western Australian iron ore mine site. The client needed an in-pit dewatering solution to discharge excess groundwater for a new section of the pit. The solution was required within eight weeks. A bore system using equipment that would suit their requirements was designed. We provided Kwikbore bore head works systems which were trailer-mounted. This would minimise dewatering and pumping downtime during removal of the existing equipment from the mining pit during blasting and installed the head works once the blasting was completed. Overall, six mobile head works systems were used, each featuring a unique plug and play design with remote telemetry system for integration with the site SCADA system. Our experienced technicians carried out onsite commissioning to effectively integrate the pumping systems into the BHP site-wide SCADA system. The project was delivered on time and on budget and operates to the specification set out in the scope of works.

The National Anzac Centre is one of Australia’s most important cultural pilgrimages. Located within Albany’s heritage listed Princess Royal Fortress, the centre overlooks the actual harbour from which over 41,000 men and woman departed Australia for the Great War. The project required a complete sewage system in a short amount of time. The system needed to handle minimal sewage flow but be prepared for high peak loadings. This is often hard to deliver, but our systems delivered a solution to ensure optimal operation.

Allied Pumps has a long history with Busselton, and in particular the famous Busselton Jetty. In 2000 we supplied a sewage pump station – designed to hang underneath the jetty under the centre. 18 years later the system is still in good condition and is testament to the high quality product working as hard today as it was when it was installed. In addition to this sewage pump station, we also supplied a concrete pump station and sewage pump station at the Underwater Observatory. More recently we supplied pump stations for the on-shore discovery centre.

The Cockburn Central Police Station required several tank and pump solutions. Initially a galvanised regular tank was recommended. However, there were design issues with the concrete slab. The station requested an in-situ concrete tank liner. The design was changed to meet this need. Allied Pumps was able to provide a turnkey solution for our client on this project, saving the client from having to engage the services of several different sub-contractors to work on various aspects of the tank installation. This enable the client to place a single order with us for all the work on the tank and supply of the pumping systems, enabling him to focus on other aspects of the project. The final project consisted of a panel tank, circulating pump pack, hot water circulator, fire pump and tank liner pack. The result was a seamless integration between the pumps and the tanks, and reliable fire protection has been the overall outcome.

The Australian Embassy in Jakarta, Indonesia required a water supply system. Because of its location, this was a very unique project. The spec required the materials to be stainless steel and fibreglass to resist corrosion. The site also needed a controller to monitor and operate water supply valves to fill tanks for use at the building. The three water supplies were the result of rainwater runoff from the roof, bore pumps and mains piping. To ensure that the specs were met, the valves were programmed to operate depending on the supply availability. The competing requirements of this project as well as working in a foreign environment created a number of challenges. We were able to rise to the challenge, through our strong organisational skills and execution of work.

Mundella was looking to reinvent an industrial filling system and outdated production line. The brief was to provide a food grade, fully compliant solution for the careful transfer of yoghurts and dairy products from vats, while maintaining constant and sensitive flow rates and meeting specific hygiene requirements. We engineered and manufactured an innovative solution to an outdated processing line using a mobile Wilden pumping package. Read on to find out how we achieved this.

Royal Perth Hospital is a 450-bed teaching hospital located on the north-eastern edge of the CBD of Perth in Western Australia. The project started with a site visit by us. We measured and discussed the design needs for the fire pump set refurbishment. The first step was to disable and remove the existing system. This removal was the same day as the new system’s delivery so there was no site storage required. The new system was then installed in one day. This was a quick turnaround time, and we were able to meet the timeframe to ensure minimal downtime.

Due to the hot weather that is common throughout the year in the Pilbara region, water stored in potable water tanks can often reach temperatures in excess of 40 degrees. This is unacceptable for applications such drinking and eye wash stations and we needed to come up with a solution to accommodate this. We also provided the fire protection for a new Sino Iron Steel Warehouse in a tight 6 week deadline. Keep an eye out for the Fire Protection provided and find out more about the Eye Wash Station below.

The Christmas Island International Airport serves visitors and residents of Christmas Island, a territory of Australia in the Indian Ocean. The building required a containerised system for its fire pump set. We were able to offer expert advice and help in the installation and usage of the system for the Christmas Island Airport personnel.

The Craft Street project involved 8 adjoining lots which required fire protection. To solve this problem, two (2) tanks measuring 5.12 m in diameter by 9.20 m high were assembled onsite and situated next to a fire pumpset in its own custom built enclosure. By collaborating, the owners of the 8 lots were able to share the costs and find a collective solution that worked for them. The short lead time was met and we were able to meet the client expectations in the provided timeframe.
Hydrant flow test kits measure water flow, static pressure, and residual pressure during testing.
Yes, Allied Pumps hydrant flow test kits are pre-calibrated on NATA test facilities and certificates are issued.
Yes, Allied Pumps supplies complete hydrant flow test kits with the components required for accurate and reliable hydrant testing.
Our jacking pumps are used in fire hydrant and fire sprinkler systems across commercial buildings, public infrastructure and high-rise developments.
Our hydrant flow test kits are used for below-ground street hydrants, above-ground hydrants, and buildings hydrants.
























































































