Our bore headworks systems have been field-tested in a range of applications, including water transfer, mine dewatering, and water supply for dust suppression operations.
Allied Pumps designs complete turn-key packages that are ready for activation upon delivery. Before dispatch all our bore headworks systems are meticulously tested in a controlled ISO 9001:2015 certified factory environment.
Our experienced Site Team can also assist with installation and integration with existing systems if required.

The Allied Pumps team uses our BIS-5000 to remove the existing bore pump from the borehole.

The new bore pump is safely lowered into the borehole using the BIS-5000.

Your preferred bore headworks system is installed and connected to the new bore pump.







Located on Connelly Street at the Greater Sports Ground is the new built recreation & leisure centre incorporating the Kellerberrin & Districts Club. This was the site of the first concrete pump station in Western Australia. When wastewater has to get to the treatment facility and gravity is not cooperating, precast concrete pump stations do the heavy lifting. Precast concrete pump stations are designed, fabricated and installed with the highest-quality materials and equipment. We installed this system in the early 1990s. Completing a project like shows how we adopt innovation in out techniques.

Formed in 1905 to obtain, treat and distribute water supplies, the Bunbury Water Board has served the people of Bunbury for over 100 years. The city’s early settlers knew of water stored naturally underground and tried to use it to replace the Collie River and the Preston River, which were the only sources of water for drinking in those days. We supplied the first variable speed system to the water authority. It’s still being used today.

The Perth City Link bus port is reconnecting Northbridge with the city centre, extending from the Perth Station to the new Perth Arena. The bus port required sufficient water storage for protection against fire. Delivering water storage in an underground situation is challenging but necessary. We had several hurdles to overcome. Our ultimate solution was to recommend our dual diesel fire protection pump set. This included suction and discharge manifolds combined with dual rectangular steel liner panel tanks. We manufactured the complete fire pumps skid at our production facility, so they could be tested at our test facility. Installing the tanks onsite was then a challenge in the tight confines of the underground plant room. The successful outcome offered a sufficient amount of water that could be dumped quickly in the case of a sudden fire.

The National Anzac Centre is one of Australia’s most important cultural pilgrimages. Located within Albany’s heritage listed Princess Royal Fortress, the centre overlooks the actual harbour from which over 41,000 men and woman departed Australia for the Great War. The project required a complete sewage system in a short amount of time. The system needed to handle minimal sewage flow but be prepared for high peak loadings. This is often hard to deliver, but our systems delivered a solution to ensure optimal operation.

The Christmas Island International Airport serves visitors and residents of Christmas Island, a territory of Australia in the Indian Ocean. The building required a containerised system for its fire pump set. We were able to offer expert advice and help in the installation and usage of the system for the Christmas Island Airport personnel.

This project was the result of a need to facilitate communication between two pump stations. One was located at Denmark High School; the other at Riverside Club. This project included supply, installation, and commission of control equipment. The objective was to pause the operation of the Riverside Club pump station when one of the pumps at the high school was operating. A dialler system was used to sync these two locations. We delivered the solution to connect these two systems which increased the efficiencies of the solutions.

Allied Pumps has a long history with Busselton, and in particular the famous Busselton Jetty. In 2000 we supplied a sewage pump station – designed to hang underneath the jetty under the centre. 18 years later the system is still in good condition and is testament to the high quality product working as hard today as it was when it was installed. In addition to this sewage pump station, we also supplied a concrete pump station and sewage pump station at the Underwater Observatory. More recently we supplied pump stations for the on-shore discovery centre.
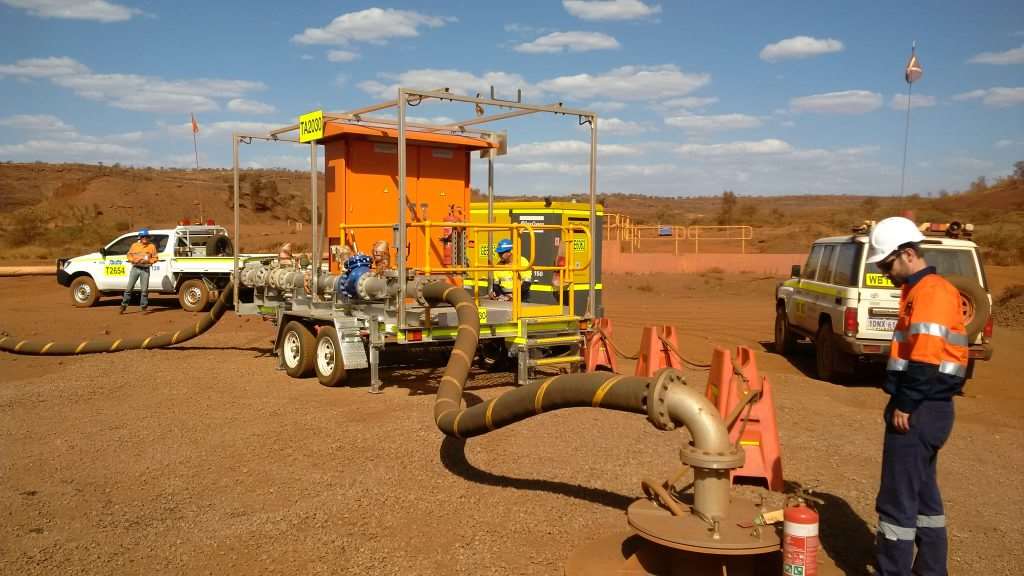
A below water table mine operation in the Shire of East Pilbara sustains the Newman Hub mining operations at a Western Australian iron ore mine site. The client needed an in-pit dewatering solution to discharge excess groundwater for a new section of the pit. The solution was required within eight weeks. A bore system using equipment that would suit their requirements was designed. We provided Kwikbore bore head works systems which were trailer-mounted. This would minimise dewatering and pumping downtime during removal of the existing equipment from the mining pit during blasting and installed the head works once the blasting was completed. Overall, six mobile head works systems were used, each featuring a unique plug and play design with remote telemetry system for integration with the site SCADA system. Our experienced technicians carried out onsite commissioning to effectively integrate the pumping systems into the BHP site-wide SCADA system. The project was delivered on time and on budget and operates to the specification set out in the scope of works.

Our client required new potable water and fire water storage tanks to be manufactured onsite. The location is particularly close to the harbour shoreline and situated in the category 5 cyclone region, which means winds can be in excess of 280 km per hr. This impacted every facet of design. We had extensive contact with suppliers to find alternative products that could withstand the aggressive environmental location. The process included a search for tank wall, nuts, and bolts all the way through to paints and roofing materials. We successfully installed all the equipment on schedule, within a 3 week period with no major disruptions or safety incidents. The tank construction was guaranteed for 25 years. The client was very satisfied with the end solution.

Station street markets were historic markets located in Subiaco that closed in 2015 after 30 years. In 2017, the site became part of a $96M redevelopment plan. We are currently working on this project constructing custom 4.70 diameter by 9.20 high fire water tanks (holding 150 kL each). These are custom specifications to meet the site’s needs. Creating custom length panels highlights our ingenuity and abilities to accommodate clients.
Allied Pumps supplies VSD skids, dewatering trailers, and aquifer reinjection skids as part of our bore headworks solutions.
Yes, Allied Pumps provide bore installation and removal using our BIS 5000. This unit allows for safe and fast bore rising and lowering.
Allied Pumps’ bore headworks packages are used for water transfer, mine dewatering, aquifer water reinjection, and water supply for dust suppression.
Yes, Allied Pumps tests all equipment using our in-house AS 2417 Test Rig (700 L/sec). Clients are invited to witness the testing in person if they like.
Yes, Allied Pumps provide custom controls for all their bore headworks systems. Our in-house electrical team seamlessly integrate the controllers into each package.


















































































