Allied Pumps designs, manufactures, and installs fire water tanks that provide a reliable water supply for fire protection systems.
Available in circular and rectangular configurations, our tanks can be customised to suit site constraints, storage requirements, and project specifications.
All our tanks are manufactured from galvanised steel panels and installed by our site team using a tank jacking system that removes the need for working at heights.
Yes, Allied Pumps manufactures fire water storage tanks in accordance with AS2304 and can supply them as part of a complete fire protection solution.
Allied Pumps supplies circular and rectangular fire water tanks in a range of capacities to suit project-specific requirements.
Yes, Allied Pumps provides installation services using a tank jacking system that eliminates the need for working at heights.
A range of accessories are available, including ladders, platforms, access hatches, tank liners, pipe connections, and monitoring systems.
Yes, Allied Pumps can supply complete fire protection packages that integrate fire water tanks with fire pumps, controllers, and associated equipment.

A residential complex in Perth required an innovative way to pump water to reduce power consumption and improve sustainability. In many new buildings, there is a push to use a single basement tank with basement pumps pressuring all the way to the top of the apartment block. However, Allied Pumps had a better solution. A small pump and tank at the basement of the apartment block transfers water to the rooftop tanks at a low flow, keeping the rooftop tank full. A smaller, variable speed pump supplies the top few floors, whilst the levels below are fed by gravity. With a roof top tank full of water at all times, even during a power outage, the system can still supply the residents with water. Smaller pumps, simpler control logic, and reduced tank capacities all kept initial costs low and provided huge benefits for the complex.

Canal Rocks Beachfront Resort sits waterfront at Smiths Beach in Yallingup. It offers beautiful accommodation for families, friends and couples visiting Yallingup and its surroundings. The facility required a fire pro pump set. We used the first AS2941-2013, which we designed, manufactured and installed the system, ensuring it met all standards and regulations. The project had its challenges since it was a first, however its successful completion enabled us to learn valuable information which will help in future installations. The project highlighted our ability to quickly learn on the job whilst successfully completing the project brief.

The City of Subiaco had an initiative to improve water quality. The focus was on reducing pollutants in Lake Mabel Talbot. The lake is in the conservation category wetland under the Environment Protection policy and functions as a Water Corporation compensating basin. The lake collects rainfall runoff from four sub-catchments, totaling 300 ha. A Gross Pollutant Trap needed to treat the entire flow prior to entering the system, and our Baffle Box was the only system to appropriately meet the design criteria. The Baffle Box was able to catch leaves and other pollutants before they could enter the lake. The result of this project was cleaner water and an improvement in the water quality.

The Christmas Island International Airport serves visitors and residents of Christmas Island, a territory of Australia in the Indian Ocean. The building required a containerised system for its fire pump set. We were able to offer expert advice and help in the installation and usage of the system for the Christmas Island Airport personnel.

The Australian Embassy in Jakarta, Indonesia required a water supply system. Because of its location, this was a very unique project. The spec required the materials to be stainless steel and fibreglass to resist corrosion. The site also needed a controller to monitor and operate water supply valves to fill tanks for use at the building. The three water supplies were the result of rainwater runoff from the roof, bore pumps and mains piping. To ensure that the specs were met, the valves were programmed to operate depending on the supply availability. The competing requirements of this project as well as working in a foreign environment created a number of challenges. We were able to rise to the challenge, through our strong organisational skills and execution of work.

Allied Pumps has a long history with Busselton, and in particular the famous Busselton Jetty. In 2000 we supplied a sewage pump station – designed to hang underneath the jetty under the centre. 18 years later the system is still in good condition and is testament to the high quality product working as hard today as it was when it was installed. In addition to this sewage pump station, we also supplied a concrete pump station and sewage pump station at the Underwater Observatory. More recently we supplied pump stations for the on-shore discovery centre.

Our client required new potable water and fire water storage tanks to be manufactured onsite. The location is particularly close to the harbour shoreline and situated in the category 5 cyclone region, which means winds can be in excess of 280 km per hr. This impacted every facet of design. We had extensive contact with suppliers to find alternative products that could withstand the aggressive environmental location. The process included a search for tank wall, nuts, and bolts all the way through to paints and roofing materials. We successfully installed all the equipment on schedule, within a 3 week period with no major disruptions or safety incidents. The tank construction was guaranteed for 25 years. The client was very satisfied with the end solution.

This job represented a challenge as the insurance company who are the insurers of the BUNGE Grain Terminal required that a pumpset built to a North American standard be used on the job, otherwise they would not grant insurance cover. Insurance cover was conditional upon compliance with a standard for the fire pump not commonly used in Australia. This meant that a fire pump had to be specially imported from North America to supply to the fire company fitting out the fire services on site. Allied Pumps were able to work with an overseas Supplier to arrange the build and testing of the fire pump off shore, in a factory in North America, then arrange airfreight of some very heavy packages at considerable cost in order to reduce time lost in transit, to minimise delays in the building construction deadline. A further challenge was that there is NO LOCAL BACK UP for the North American controllers. Allied Pumps was able to rise to the occasion and overcome this challenge by our highly experienced technicians making contact with an overseas electrical technician to gain the knowledge necessary to overcome certain control panel commissioning obstacles. A fine outcome on a very challenging job!

Located on Connelly Street at the Greater Sports Ground is the new built recreation & leisure centre incorporating the Kellerberrin & Districts Club. This was the site of the first concrete pump station in Western Australia. When wastewater has to get to the treatment facility and gravity is not cooperating, precast concrete pump stations do the heavy lifting. Precast concrete pump stations are designed, fabricated and installed with the highest-quality materials and equipment. We installed this system in the early 1990s. Completing a project like shows how we adopt innovation in out techniques.
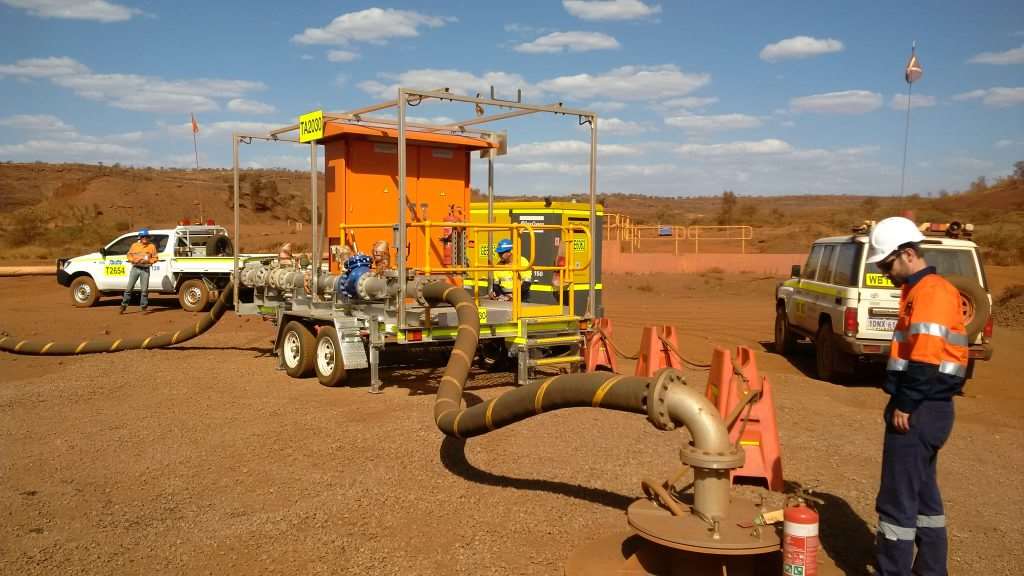
A below water table mine operation in the Shire of East Pilbara sustains the Newman Hub mining operations at a Western Australian iron ore mine site. The client needed an in-pit dewatering solution to discharge excess groundwater for a new section of the pit. The solution was required within eight weeks. A bore system using equipment that would suit their requirements was designed. We provided Kwikbore bore head works systems which were trailer-mounted. This would minimise dewatering and pumping downtime during removal of the existing equipment from the mining pit during blasting and installed the head works once the blasting was completed. Overall, six mobile head works systems were used, each featuring a unique plug and play design with remote telemetry system for integration with the site SCADA system. Our experienced technicians carried out onsite commissioning to effectively integrate the pumping systems into the BHP site-wide SCADA system. The project was delivered on time and on budget and operates to the specification set out in the scope of works.
























































































