





























































OVERVIEW
On-Site Project Solutions
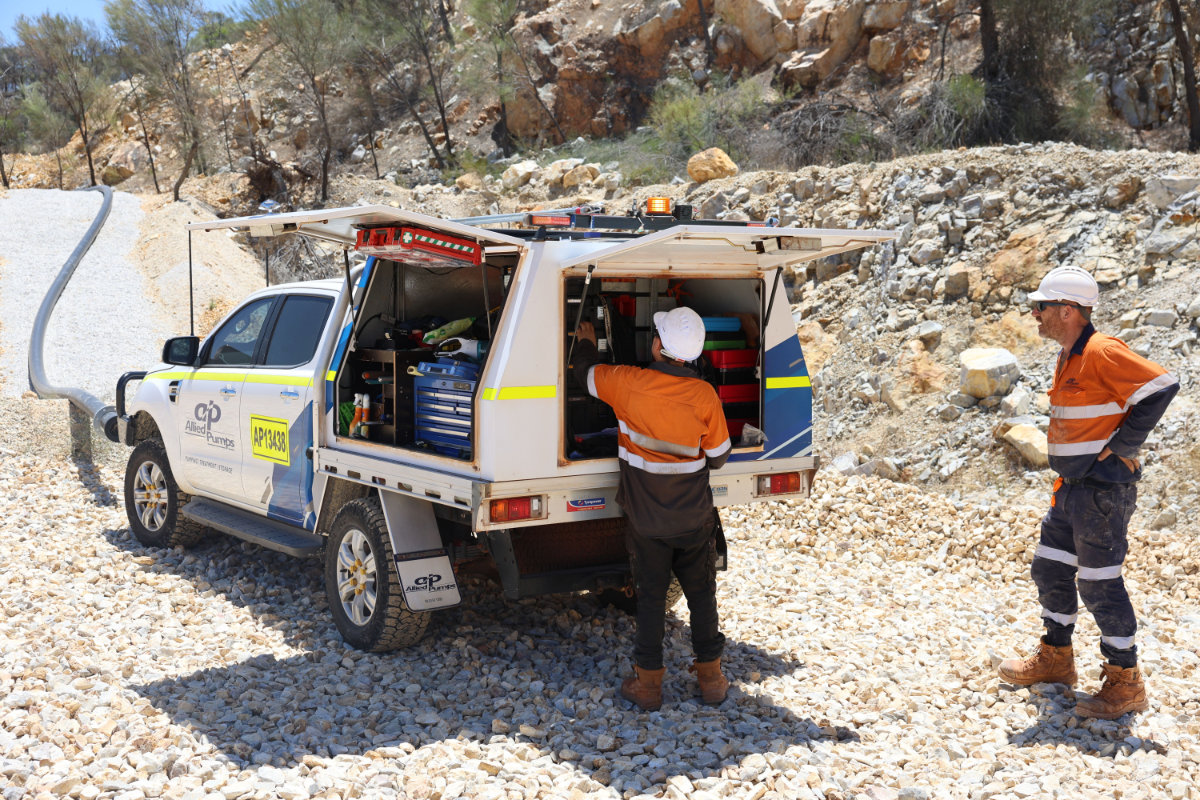
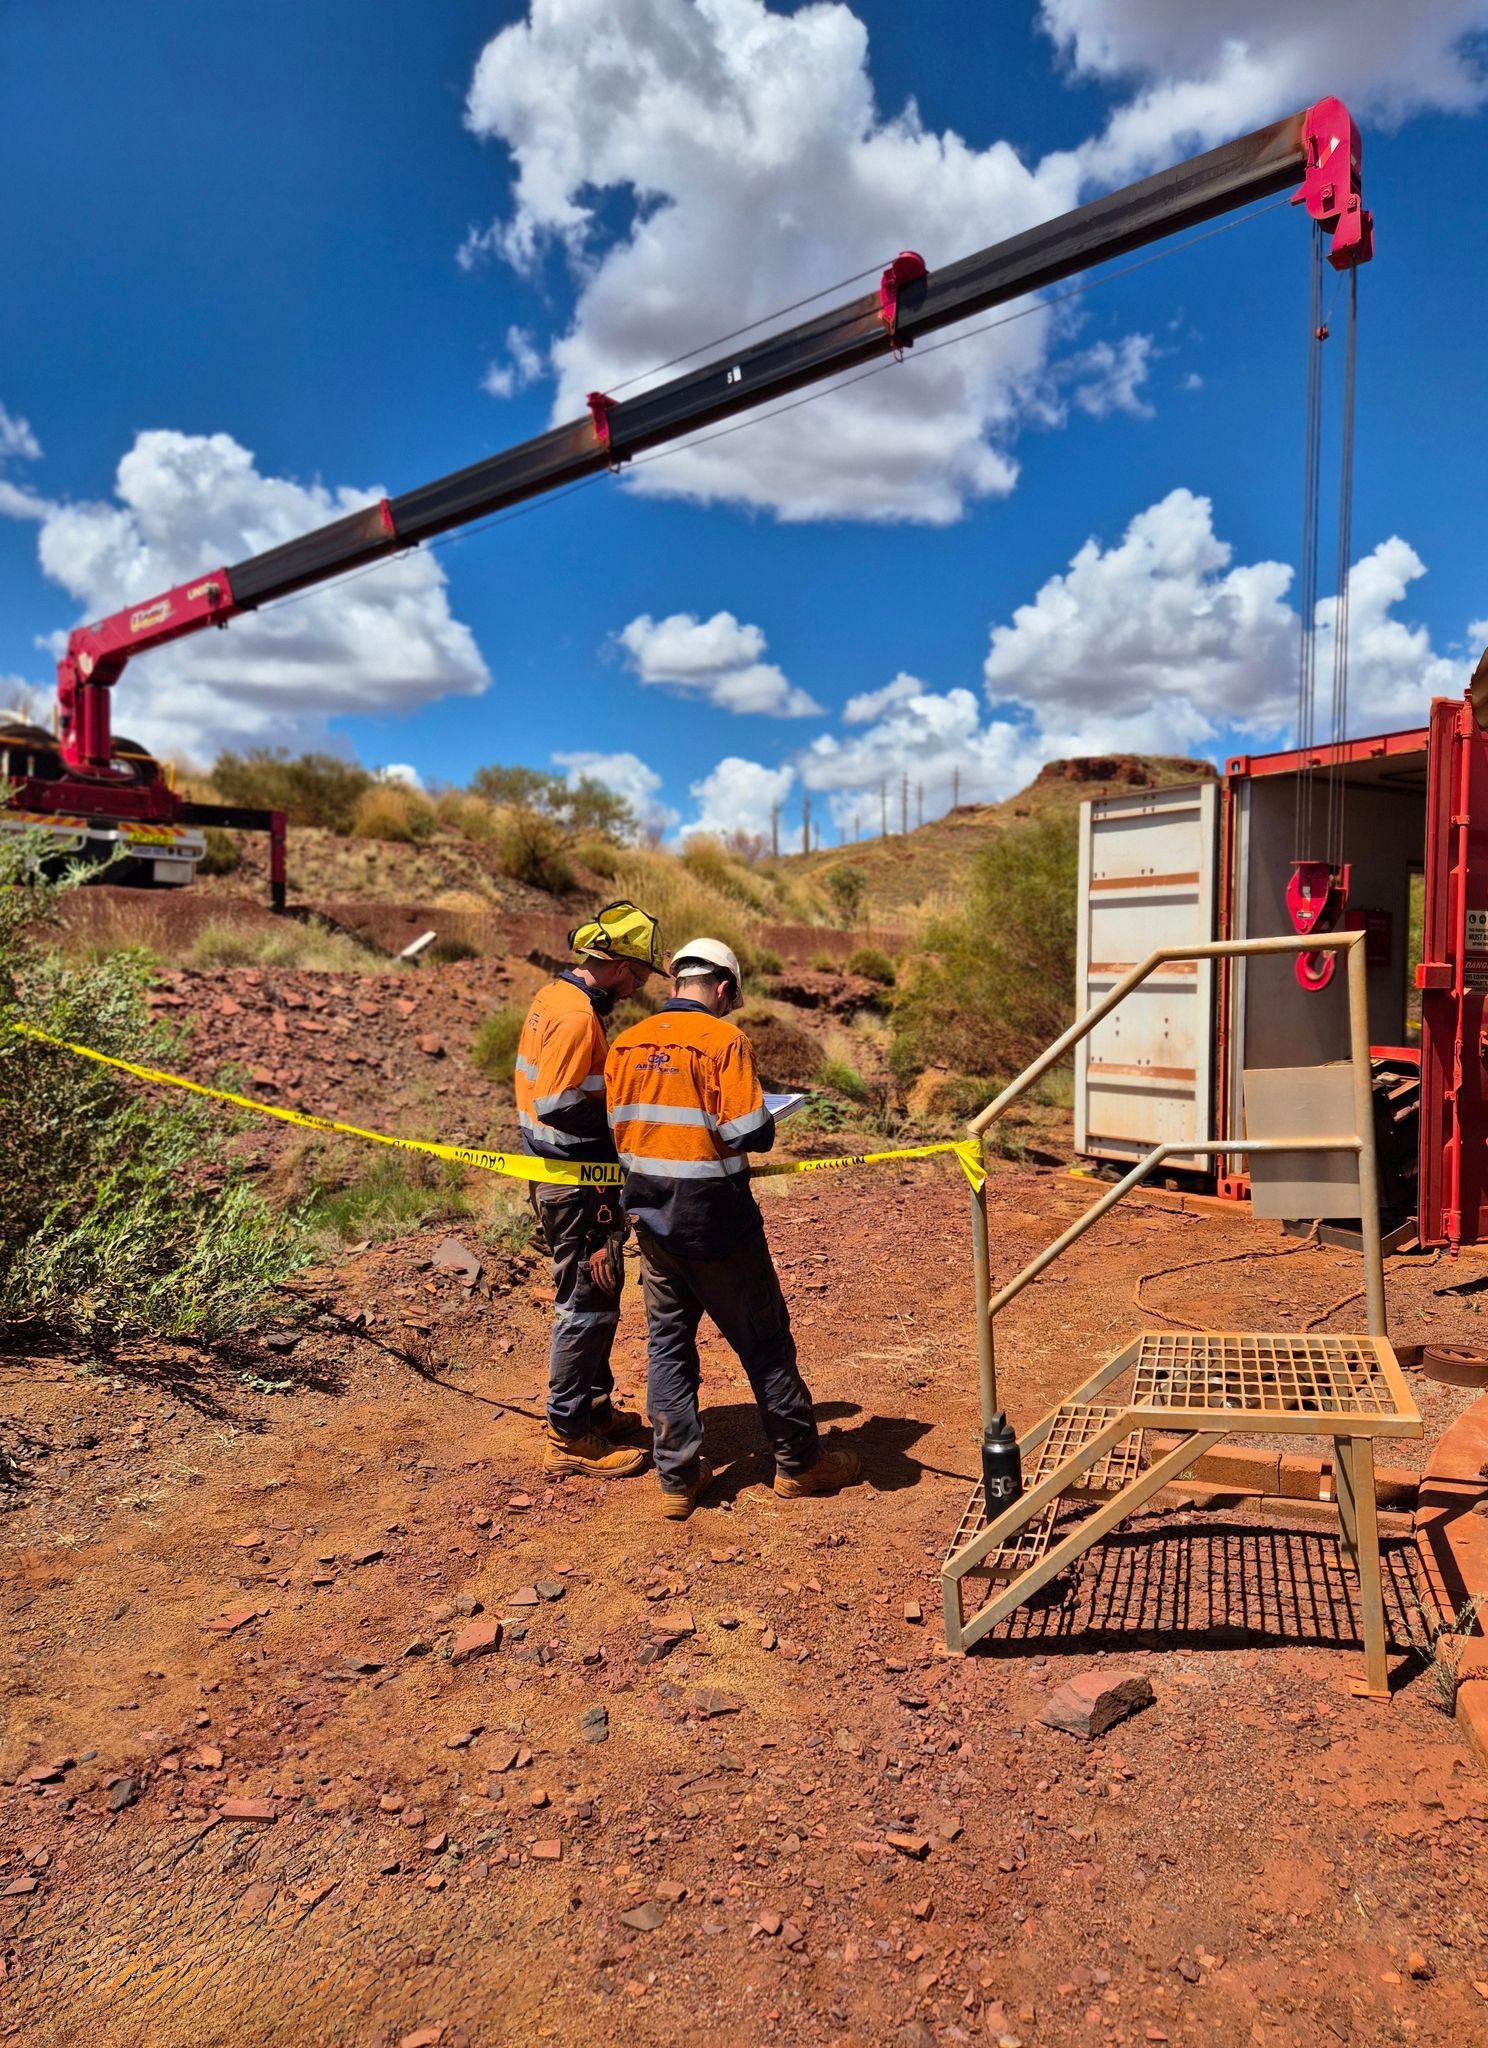
Allied Site is a specialised department of Allied Pumps, delivering on-site installations across the mining and industrial sectors with a focus on precision, efficiency and safety.
37
Since 1989
37 Years of Innovation & Commitment
PUMP REPAIRS
Complete Project Services, All Under One Roof
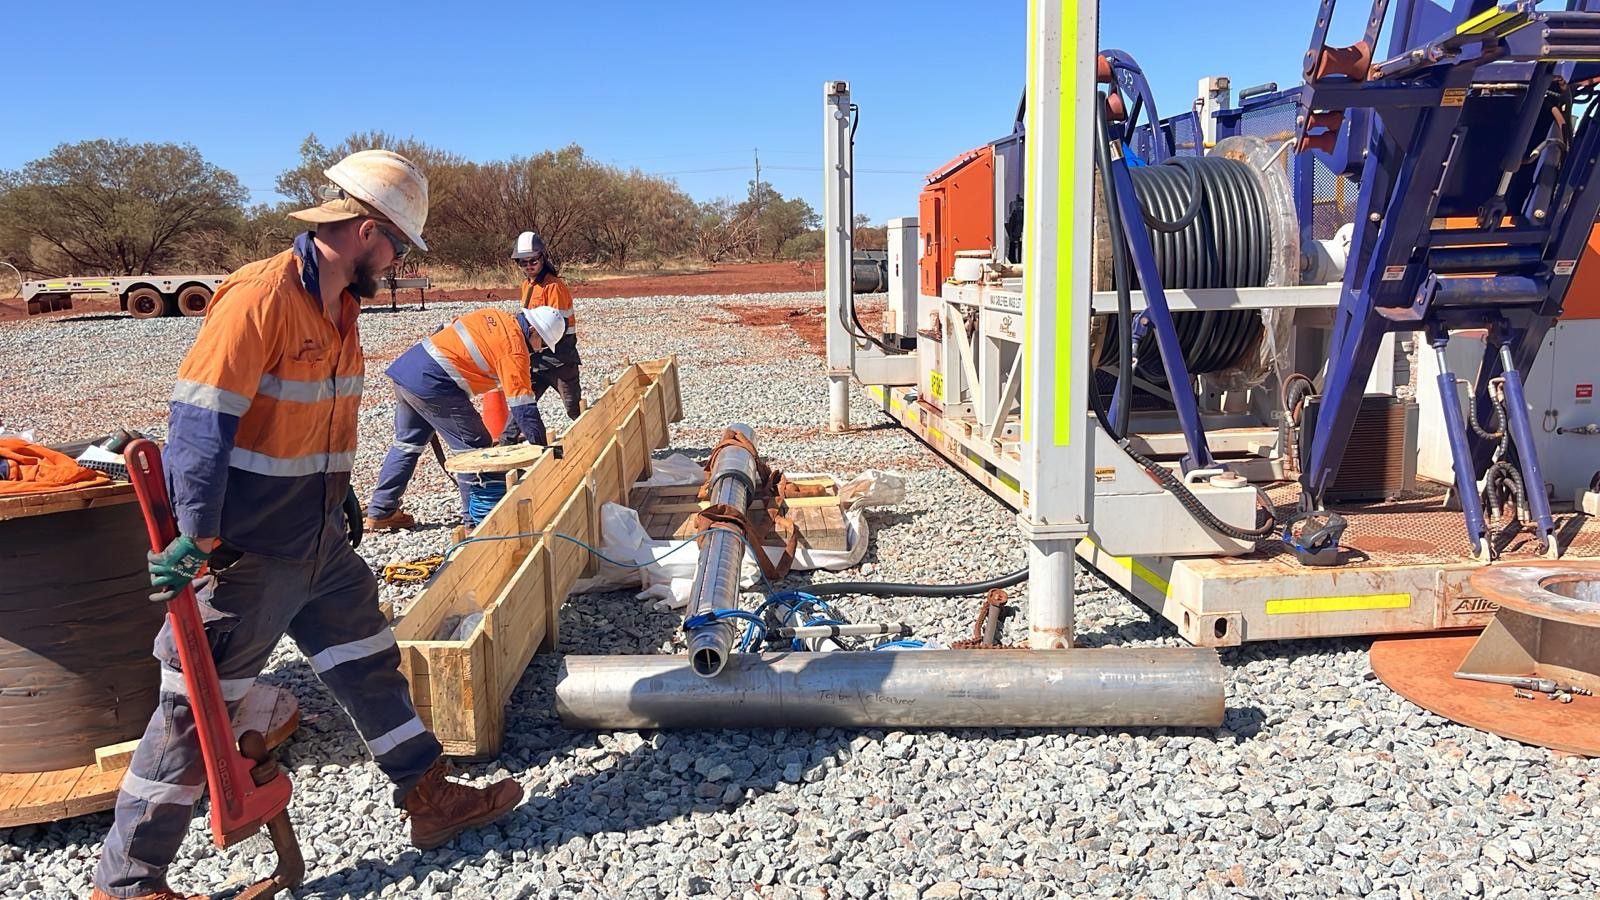
From design and fabrication through to installation and commissioning, Allied Site provides complete project support backed by engineers, designers, electricians, plumbers, mechanical fitters and experienced site personnel.
Safety First
Allied Site adheres to the latest safety regulations, with many of our staff members being S26 certified. Our experienced site team ensures that all pumping equipment, systems, and controls are installed in compliance with manufacturers’ specifications.
ISO-Certified
We continually review all policies, processes and procedures our HSEQ System to ensure it is in accordance with the ISO 9001:2015; ISO 45001:2018 and ISO 14001:2015 standards. We monitor the system through internal and external audits to retain Certification status.
OUR BENEFITS
Why Allied Site?
Working with a single supplier and installer helps eliminate scope gaps, improve equipment interconnectivity, and provide a more complete warranty.
Eliminates scope gaps and disputes between equipment supplier and installer.
S26 certified staff capable of completing both large-scale and small-scale projects.
A more complete warranty when equipment is supplied & installed by the same company.
Proven track record of working with mining clients and completing mine spec work.
Equipment built in WA to meet the harsh conditions of the Pilbara, Kimberly & South West.
Ensures all interconnected equipment interfaces with each other.
ENQUIRE
Discuss Your Next Site Project
From design and fabrication through to installation and commissioning, Allied Site has the resources and technical expertise to deliver complete project solutions under one roof.
OUR FACILITIIES
We Are Next Door to You
Allied Pumps operates from its headquarters in Canning Vale, supported by facilities in Albany, Kalgoorlie, Darwin, Sydney and Melbourne.
For mining operations in the Pilbara, our Newman Depot provides an additional local base for Allied Site, helping us mobilise personnel, equipment, and project support closer to site.
PROJECTS
Our Recent Projects
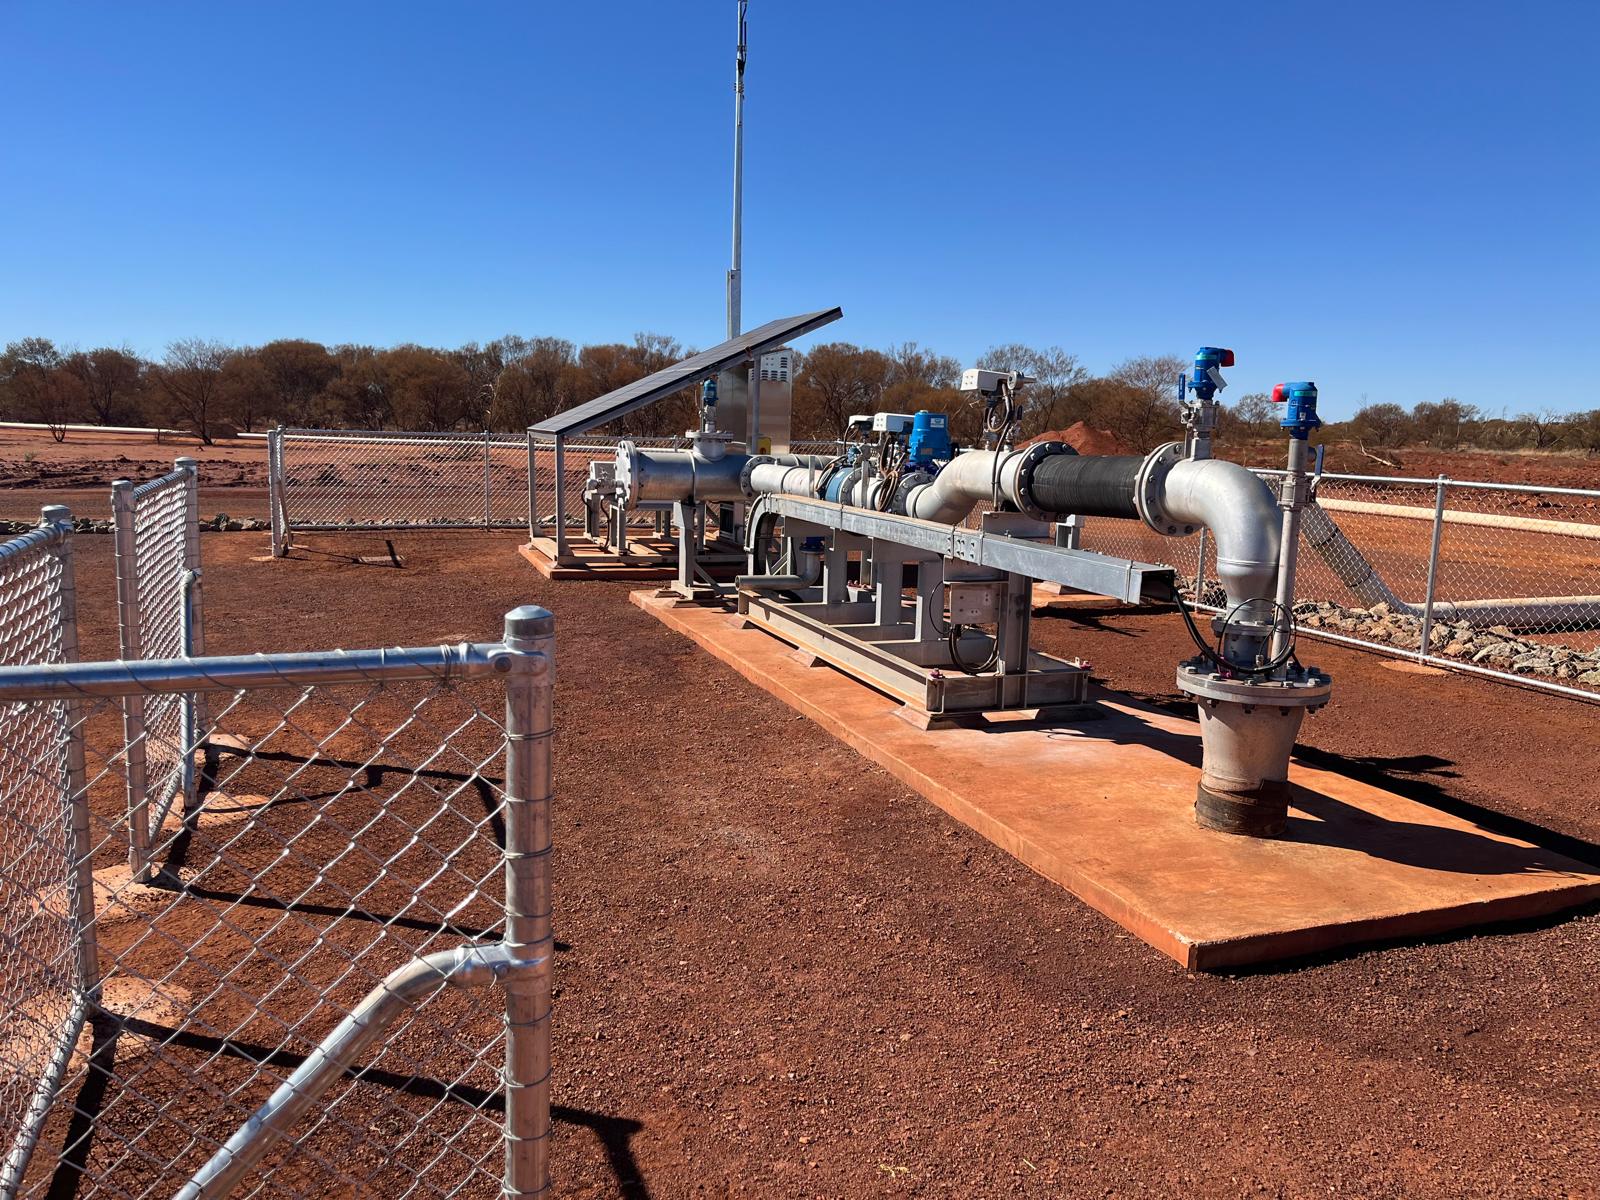
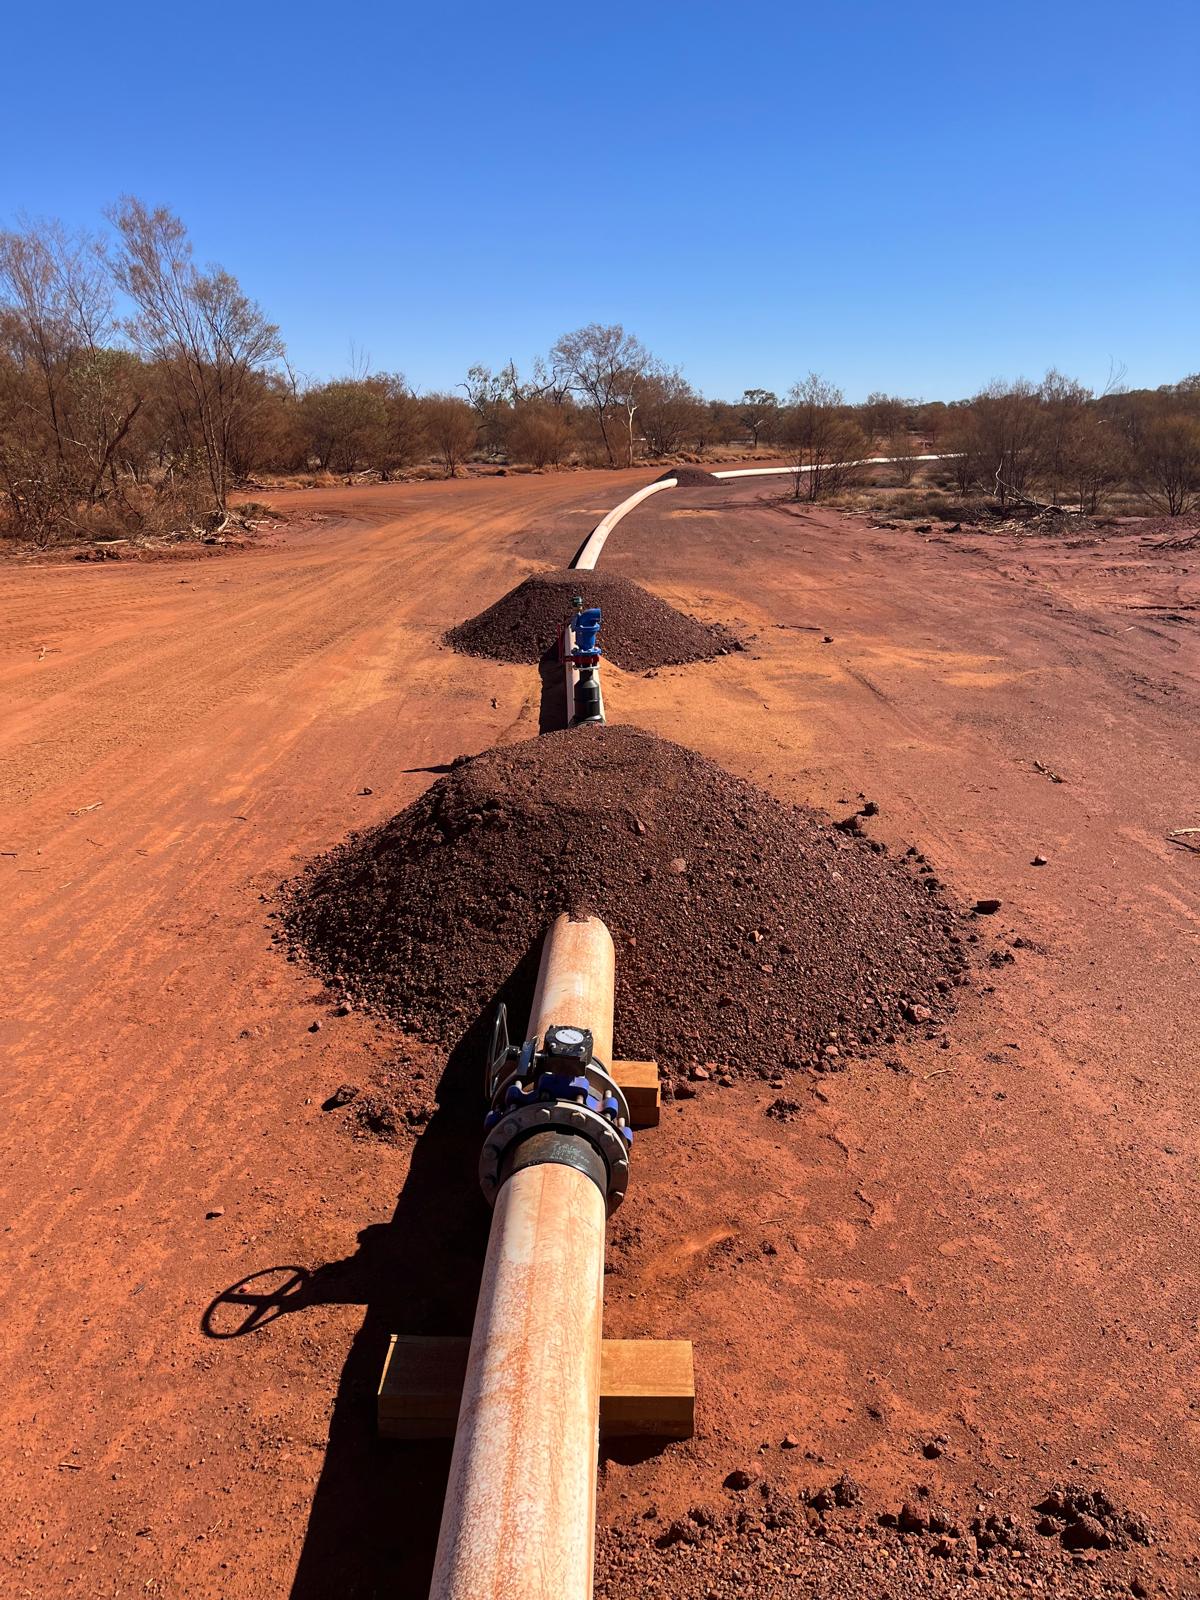
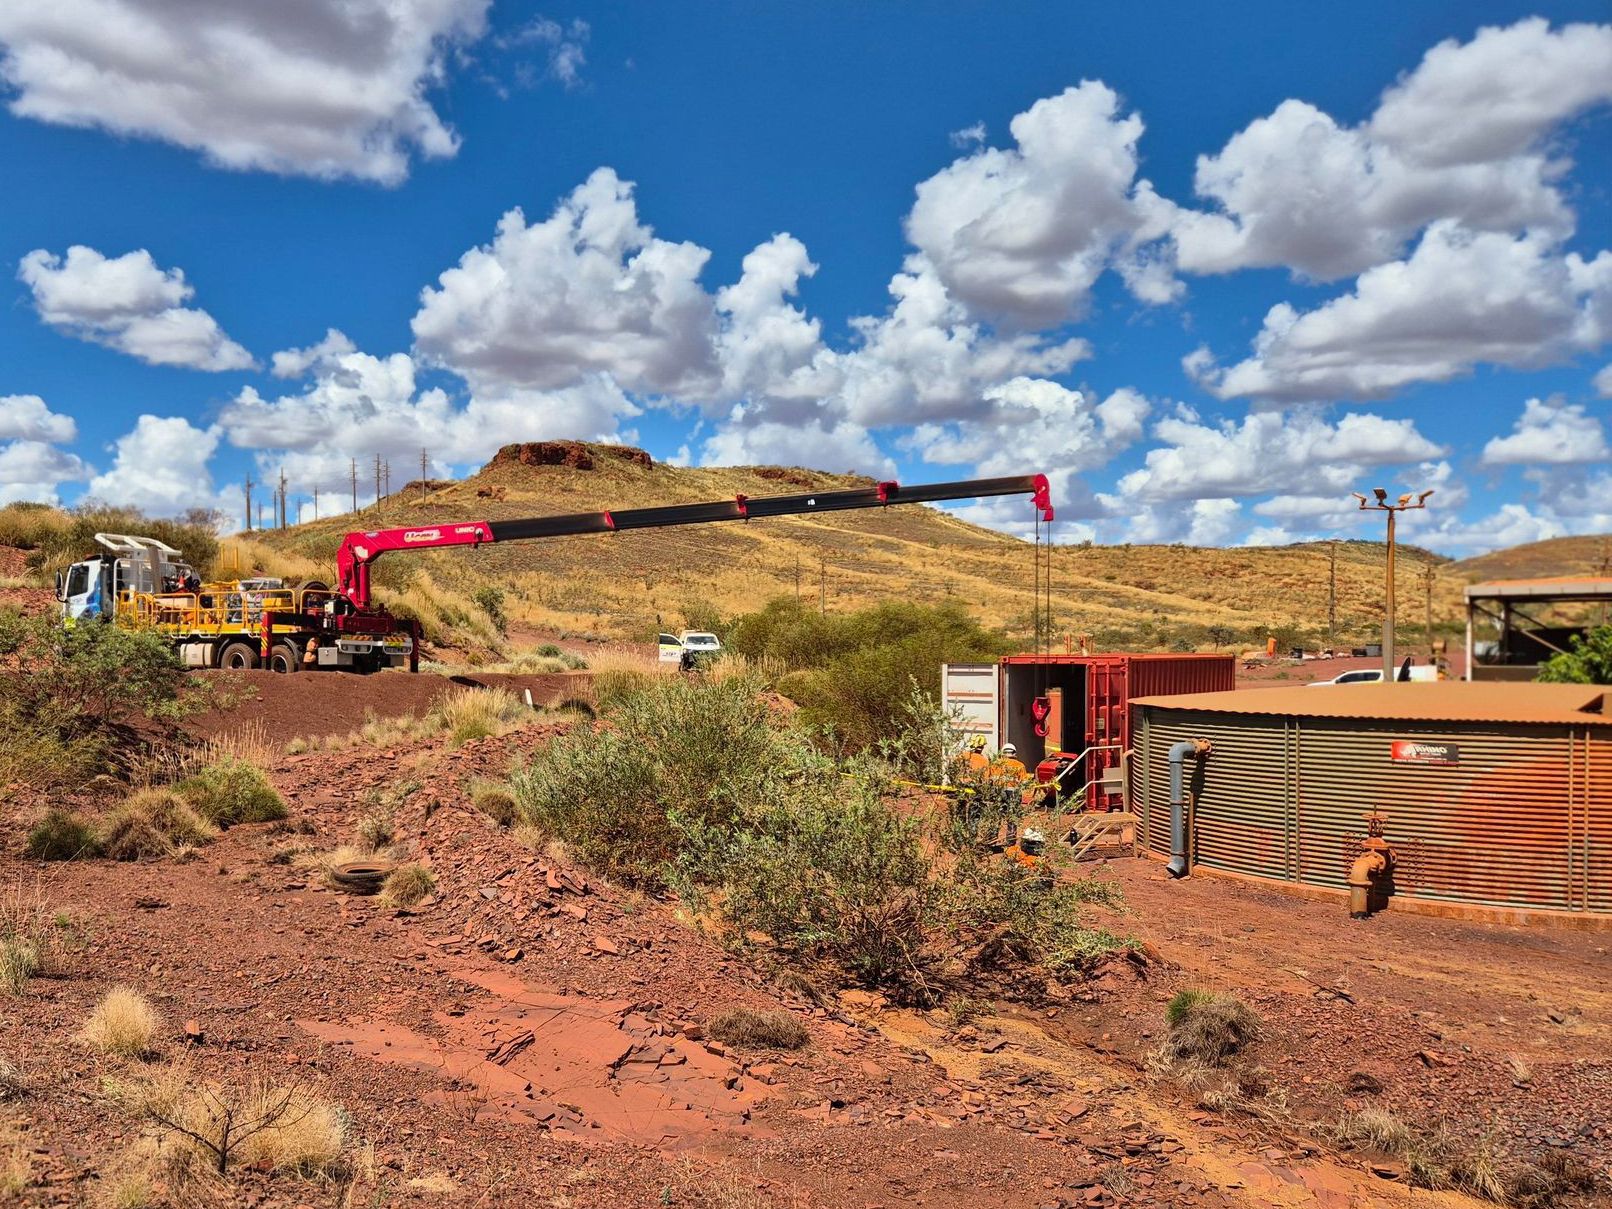
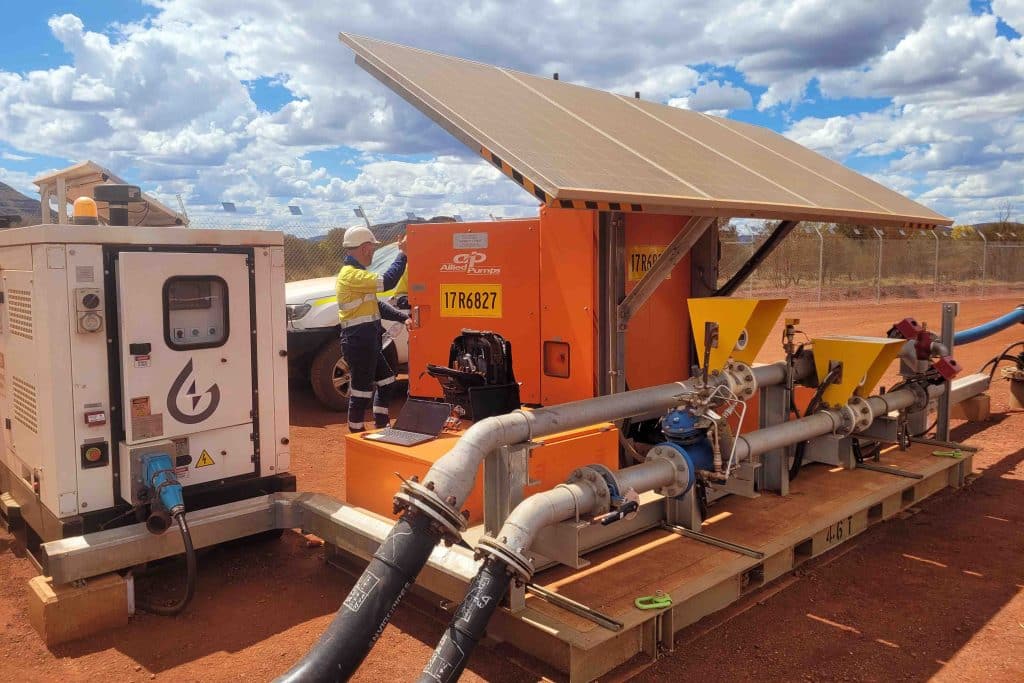
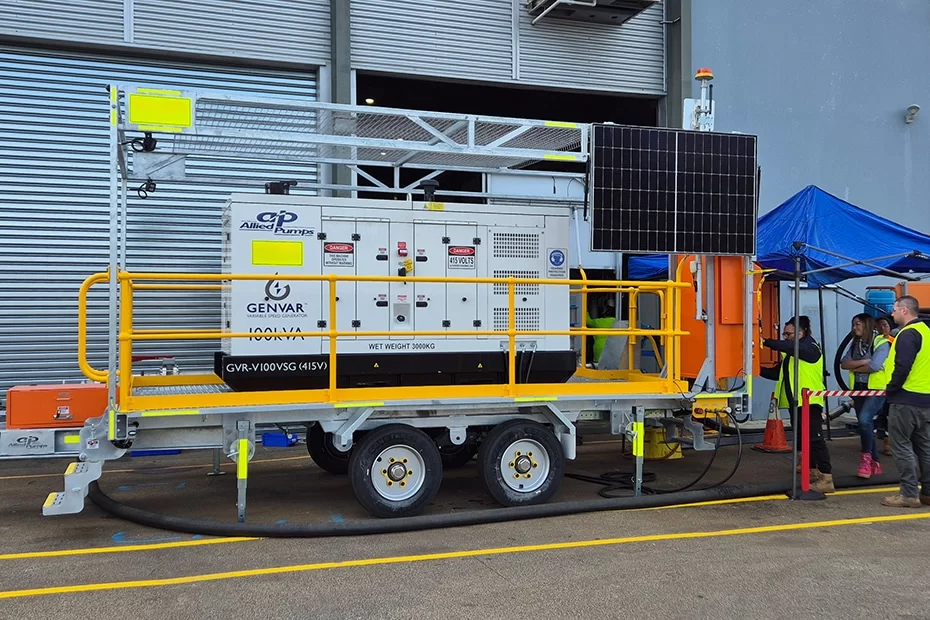
Explore Allied Site projects across water treatment, bore fields, pumping systems and storage infrastructure.
January 21, 2021
“Teamwork makes the dream work” has never rung truer than when it comes to the team here at Allied Pumps.
November 18, 2024
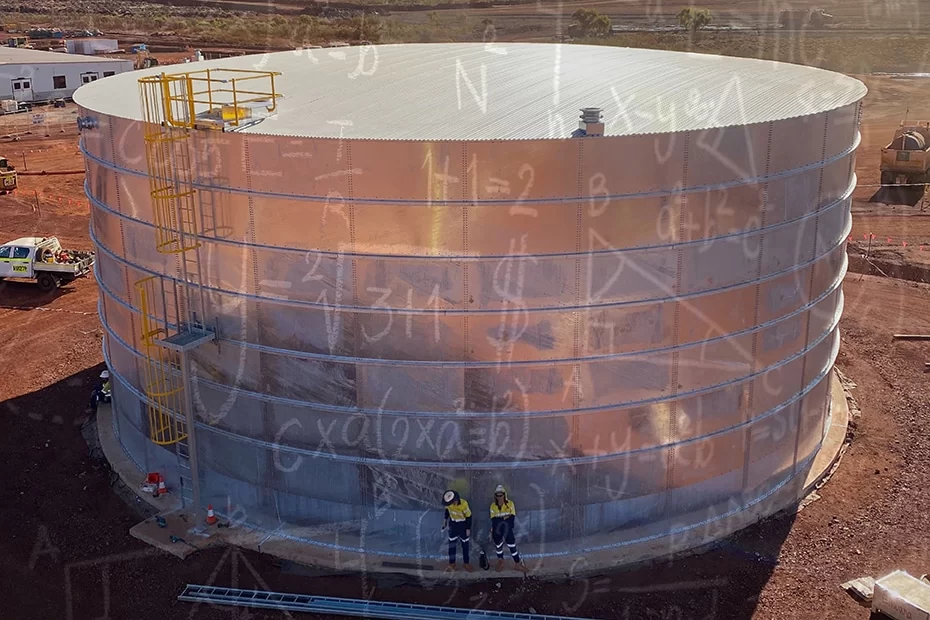
If you are asking yourself “what size water tank do I need?” then you have come to the right place.
March 14, 2024
The Australian mining industry faces formidable water management challenges due to its extensive need for water and the country’s arid
September 20, 2017
Innovation is what drives progress. New ideas and the ability to implement them successfully are essential for bringing new products
November 20, 2025
One of the biggest decisions mining operators face is choosing between a Fixed Speed Drive and a Variable Speed Drive
November 14, 2017
Allied Pumps is a leader in purpose-built hydraulic pumping and quality treatment systems. We can store any quantity and have
November 21, 2016
Recently Allied Pumps participated in the national R U OK initiative that focusses on suicide prevention in Australia. R U
May 30, 2018
A recent World Health Organization study detailing elevated levels of micro-plastics in bottled water shows we may be witnessing a
The Allied Pump range of Trolley Pumps are engineered to cater for the growing demand for a flexible solution to
As one of the leading manufacturers of compliant* complete packaged fire pumps in Australia we are often called upon to


![[Pyrokos] Fire Pump Controller](https://alliedpumps.com.au/wp-content/uploads/2020/06/Pyrokos-Fire-Pump-Controller-768x512.jpg.webp)