Allied Pumps provides total package solutions for temporary and permanent municipal pump station requirements. Dedicated precast concrete pump pits are available in 1800 mm, 2250 mm, and 3200 mm diameter configurations.
Each municipal pump system can be fully fitted with authority-specified accessories, including pipework, valves, ladders, guide rails, mounts, chains, and valve chamber drainage.
Standard packages can incorporate Grundfos, Sulzer, Corde, with alternative pump options available where required.

The Christmas Island International Airport serves visitors and residents of Christmas Island, a territory of Australia in the Indian Ocean. The building required a containerised system for its fire pump set. We were able to offer expert advice and help in the installation and usage of the system for the Christmas Island Airport personnel.

Located on the Burswood Peninsula, the Optus Stadium is part of a large redevelopment that has become a draw card to thousands of people. However, as with all new developments there was a significant change to the existing landscape. Part of the Optus Stadium is bounded by the Swan River and river traffic, some of the retaining walls and steel piles on the water’s edge which could be seen from the water and needed to be addressed which could not be achieved using a land based planting scheme or additional construction. Allied Pumps created an environmentally sound and sustainable floating treatment wetland that can be configured in rafts of endless configurations. They can fit any existing space or water body shape and can operate in fluctuating water levels which was an essential requirement for this project. While the floating treatment wetlands are primarily a water treatment tool, they have the added bonus of being visually appealing with the use of wetland sedges, rushes and grasses providing fast and easy to install beautification options.

Blockages occur fairly regularly at Graylands Hospital, Western Australia’s largest mental health facility. Objects and clothing were often being introduced into the plumbing system. With 1,053 fixtures, the system needed help breaking up these foreign objects. Two of their grinder pumps were not properly handling foreign objects. After much investigation, the most practical option was to install a channel grinder in the existing mechanical screening pit. We designed specialised guiderails from 316 stainless steel. They were built in-house to suit the existing concrete structure. This solved the issue and eliminated peak flow blockages. The system has now been up and running for 24 months with no issues.

This job represented a challenge as the insurance company who are the insurers of the BUNGE Grain Terminal required that a pumpset built to a North American standard be used on the job, otherwise they would not grant insurance cover. Insurance cover was conditional upon compliance with a standard for the fire pump not commonly used in Australia. This meant that a fire pump had to be specially imported from North America to supply to the fire company fitting out the fire services on site. Allied Pumps were able to work with an overseas Supplier to arrange the build and testing of the fire pump off shore, in a factory in North America, then arrange airfreight of some very heavy packages at considerable cost in order to reduce time lost in transit, to minimise delays in the building construction deadline. A further challenge was that there is NO LOCAL BACK UP for the North American controllers. Allied Pumps was able to rise to the occasion and overcome this challenge by our highly experienced technicians making contact with an overseas electrical technician to gain the knowledge necessary to overcome certain control panel commissioning obstacles. A fine outcome on a very challenging job!
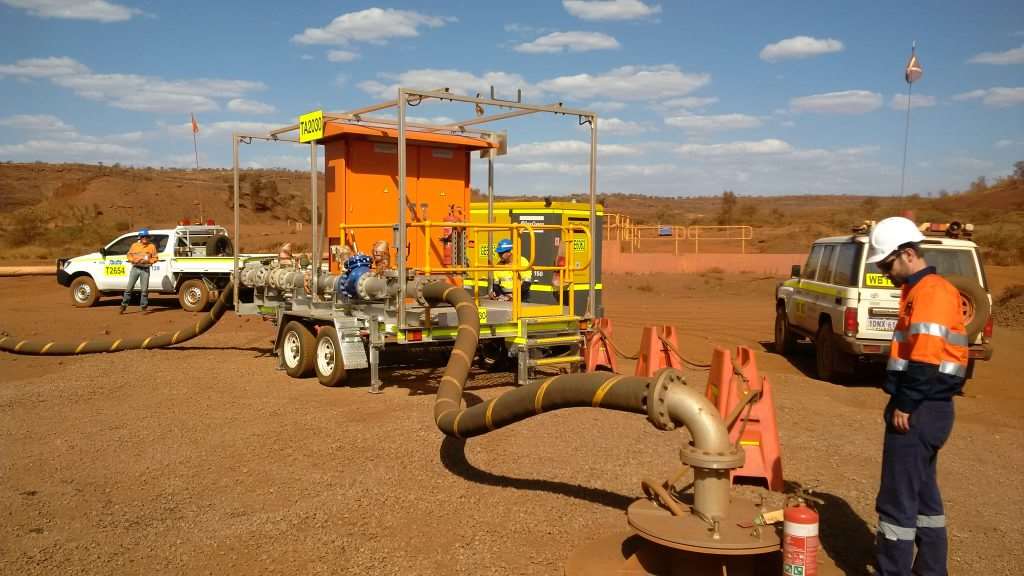
A below water table mine operation in the Shire of East Pilbara sustains the Newman Hub mining operations at a Western Australian iron ore mine site. The client needed an in-pit dewatering solution to discharge excess groundwater for a new section of the pit. The solution was required within eight weeks. A bore system using equipment that would suit their requirements was designed. We provided Kwikbore bore head works systems which were trailer-mounted. This would minimise dewatering and pumping downtime during removal of the existing equipment from the mining pit during blasting and installed the head works once the blasting was completed. Overall, six mobile head works systems were used, each featuring a unique plug and play design with remote telemetry system for integration with the site SCADA system. Our experienced technicians carried out onsite commissioning to effectively integrate the pumping systems into the BHP site-wide SCADA system. The project was delivered on time and on budget and operates to the specification set out in the scope of works.

Canal Rocks Beachfront Resort sits waterfront at Smiths Beach in Yallingup. It offers beautiful accommodation for families, friends and couples visiting Yallingup and its surroundings. The facility required a fire pro pump set. We used the first AS2941-2013, which we designed, manufactured and installed the system, ensuring it met all standards and regulations. The project had its challenges since it was a first, however its successful completion enabled us to learn valuable information which will help in future installations. The project highlighted our ability to quickly learn on the job whilst successfully completing the project brief.

Our client required new potable water and fire water storage tanks to be manufactured onsite. The location is particularly close to the harbour shoreline and situated in the category 5 cyclone region, which means winds can be in excess of 280 km per hr. This impacted every facet of design. We had extensive contact with suppliers to find alternative products that could withstand the aggressive environmental location. The process included a search for tank wall, nuts, and bolts all the way through to paints and roofing materials. We successfully installed all the equipment on schedule, within a 3 week period with no major disruptions or safety incidents. The tank construction was guaranteed for 25 years. The client was very satisfied with the end solution.

Allied Pumps has a long history with Busselton, and in particular the famous Busselton Jetty. In 2000 we supplied a sewage pump station – designed to hang underneath the jetty under the centre. 18 years later the system is still in good condition and is testament to the high quality product working as hard today as it was when it was installed. In addition to this sewage pump station, we also supplied a concrete pump station and sewage pump station at the Underwater Observatory. More recently we supplied pump stations for the on-shore discovery centre.

Allied Pumps creates insulated circular steel panel liner tank for the Karratha Health Campus to meet clients cold water requirements. We were able to meet the client’s stringent requirements to produce a cost effective, potable water tank that could withstand the extreme weather conditions. Rising to the challenge, this project was Allied Pumps first insulated circular steel panel liner tank complete with a cold water circulating program.

We were recently involved in supplying fire protection for Perth Airport. View the video to see the testing DFES conducted at the facilities in March 2017.
Allied Pumps’ municipal pump stations come equipped with dedicated precast concrete pump pits in 1800 mm, 2250 mm, and 3200 mm diameter configurations.
Allied Pumps’ municipal pump stations can include pumps, pipework, valves, ladders, guide rails, mounts, chains, and valve chamber drainage, depending on authority and project specifications.
Standard packages can incorporate Grundfos, Sulzer, Corde, or other authority-approved pumps are available on request.
Yes, Allied Pumps’ municipal pump stations include a large, sealed integral valve chamber with separate access through a cast iron cover incorporated into the main precast slab.
The Allied Pumps’ municipal pump package provides single responsibility, simplifies specifying and ordering, and reduces the amount of work required on site.
























































































