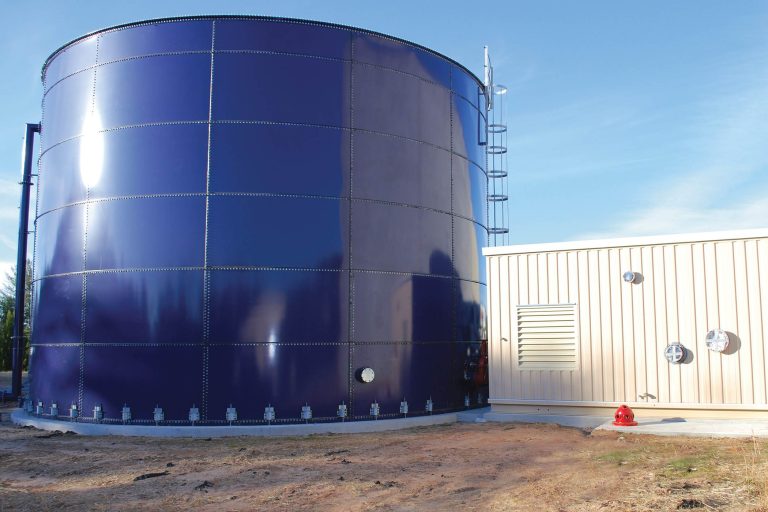
Designed for performance in demanding environments, Allied Pumps’ industrial water tanks provide robust, high-capacity storage for both mines sites and process plants.
Manufactured to rigorous Australian Standards using corrosion-resistant materials, they are built to withstand extreme conditions.
With flexible configurations and capacities, these tanks can integrate efficiently with pumps to provide reliable water supply for potable, process, wastewater, and fire protection.

The tank jacks are equipped to every vertical joint around the tank.


All external fittings and accessories are installed once the tank is at specified height.



The Australian Embassy in Jakarta, Indonesia required a water supply system. Because of its location, this was a very unique project. The spec required the materials to be stainless steel and fibreglass to resist corrosion. The site also needed a controller to monitor and operate water supply valves to fill tanks for use at the building. The three water supplies were the result of rainwater runoff from the roof, bore pumps and mains piping. To ensure that the specs were met, the valves were programmed to operate depending on the supply availability. The competing requirements of this project as well as working in a foreign environment created a number of challenges. We were able to rise to the challenge, through our strong organisational skills and execution of work.

The Perth City Link bus port is reconnecting Northbridge with the city centre, extending from the Perth Station to the new Perth Arena. The bus port required sufficient water storage for protection against fire. Delivering water storage in an underground situation is challenging but necessary. We had several hurdles to overcome. Our ultimate solution was to recommend our dual diesel fire protection pump set. This included suction and discharge manifolds combined with dual rectangular steel liner panel tanks. We manufactured the complete fire pumps skid at our production facility, so they could be tested at our test facility. Installing the tanks onsite was then a challenge in the tight confines of the underground plant room. The successful outcome offered a sufficient amount of water that could be dumped quickly in the case of a sudden fire.

This job represented a challenge as the insurance company who are the insurers of the BUNGE Grain Terminal required that a pumpset built to a North American standard be used on the job, otherwise they would not grant insurance cover. Insurance cover was conditional upon compliance with a standard for the fire pump not commonly used in Australia. This meant that a fire pump had to be specially imported from North America to supply to the fire company fitting out the fire services on site. Allied Pumps were able to work with an overseas Supplier to arrange the build and testing of the fire pump off shore, in a factory in North America, then arrange airfreight of some very heavy packages at considerable cost in order to reduce time lost in transit, to minimise delays in the building construction deadline. A further challenge was that there is NO LOCAL BACK UP for the North American controllers. Allied Pumps was able to rise to the occasion and overcome this challenge by our highly experienced technicians making contact with an overseas electrical technician to gain the knowledge necessary to overcome certain control panel commissioning obstacles. A fine outcome on a very challenging job!

Allied Pumps creates insulated circular steel panel liner tank for the Karratha Health Campus to meet clients cold water requirements. We were able to meet the client’s stringent requirements to produce a cost effective, potable water tank that could withstand the extreme weather conditions. Rising to the challenge, this project was Allied Pumps first insulated circular steel panel liner tank complete with a cold water circulating program.

Our client required new potable water and fire water storage tanks to be manufactured onsite. The location is particularly close to the harbour shoreline and situated in the category 5 cyclone region, which means winds can be in excess of 280 km per hr. This impacted every facet of design. We had extensive contact with suppliers to find alternative products that could withstand the aggressive environmental location. The process included a search for tank wall, nuts, and bolts all the way through to paints and roofing materials. We successfully installed all the equipment on schedule, within a 3 week period with no major disruptions or safety incidents. The tank construction was guaranteed for 25 years. The client was very satisfied with the end solution.

The Cockburn Central Police Station required several tank and pump solutions. Initially a galvanised regular tank was recommended. However, there were design issues with the concrete slab. The station requested an in-situ concrete tank liner. The design was changed to meet this need. Allied Pumps was able to provide a turnkey solution for our client on this project, saving the client from having to engage the services of several different sub-contractors to work on various aspects of the tank installation. This enable the client to place a single order with us for all the work on the tank and supply of the pumping systems, enabling him to focus on other aspects of the project. The final project consisted of a panel tank, circulating pump pack, hot water circulator, fire pump and tank liner pack. The result was a seamless integration between the pumps and the tanks, and reliable fire protection has been the overall outcome.

Due to the hot weather that is common throughout the year in the Pilbara region, water stored in potable water tanks can often reach temperatures in excess of 40 degrees. This is unacceptable for applications such drinking and eye wash stations and we needed to come up with a solution to accommodate this. We also provided the fire protection for a new Sino Iron Steel Warehouse in a tight 6 week deadline. Keep an eye out for the Fire Protection provided and find out more about the Eye Wash Station below.

It’s been 25 years, and the Bickley Booster Pump Station is still going strong. In 1992, we took on this project. This challenge began with the need to solve a low-pressure problem in the Orange Grove area. A dual pump system operating on a variable speed control was installed. This included the base, pipework, valves, control system and pressure vessel. The pump set is still functioning correctly and addressing the original issue. This project represents the quality and endurance of our pump systems.
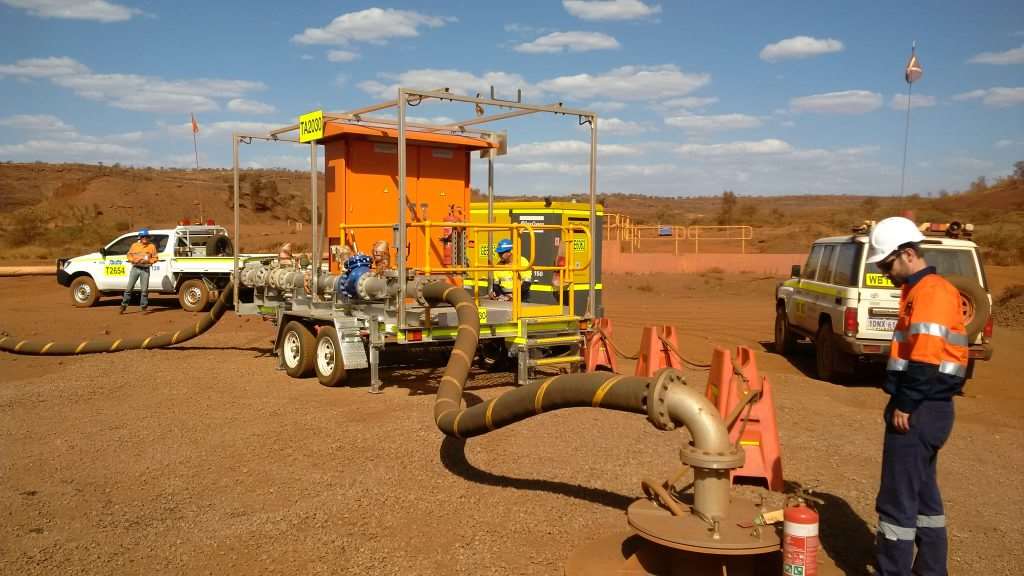
A below water table mine operation in the Shire of East Pilbara sustains the Newman Hub mining operations at a Western Australian iron ore mine site. The client needed an in-pit dewatering solution to discharge excess groundwater for a new section of the pit. The solution was required within eight weeks. A bore system using equipment that would suit their requirements was designed. We provided Kwikbore bore head works systems which were trailer-mounted. This would minimise dewatering and pumping downtime during removal of the existing equipment from the mining pit during blasting and installed the head works once the blasting was completed. Overall, six mobile head works systems were used, each featuring a unique plug and play design with remote telemetry system for integration with the site SCADA system. Our experienced technicians carried out onsite commissioning to effectively integrate the pumping systems into the BHP site-wide SCADA system. The project was delivered on time and on budget and operates to the specification set out in the scope of works.

The Craft Street project involved 8 adjoining lots which required fire protection. To solve this problem, two (2) tanks measuring 5.12 m in diameter by 9.20 m high were assembled onsite and situated next to a fire pumpset in its own custom built enclosure. By collaborating, the owners of the 8 lots were able to share the costs and find a collective solution that worked for them. The short lead time was met and we were able to meet the client expectations in the provided timeframe.

A below-water-table mine in East Pilbara required rapid groundwater removal under strict site specs. Allied Pumps engineered six mobile bore headworks systems with telemetry and SCADA integration, enabling efficient dewatering while minimising disruption during active mining.

The remote Pilbara mine required 24/7 dewatering with limited access, high diesel use, and no power for controls. Allied Pumps supplied diesel transfer skids, a 5kL/62kL fuel system, and solar telemetry, enabling SCADA monitoring, lower fuel logistics, and reliable flow control.

Challenged with harsh Pilbara conditions and saline groundwater, the client needed a compliant bore field with SCADA integration. Allied Pumps delivered 24 skid-mounted systems with 316 stainless steel pumps and telemetry, completing installation in 24 weeks and enabling reliable raw water supply.
Allied Pumps’ industrial water tanks are manufactured from panels made of galvanised steel, hot-dip galvanised steel, glass fused steel, and epoxy coated steel.
Sizing for Allied Pumps’ industrial water tanks ranges from 10kL to 30ML. Please reach out to our team if you are looking for other sizes.
Yes, Allied Pumps’ industrial water tanks are designed to meet Australian Standards like AS2304 (Fire Protection) and AS1170 (Wind Loads).
Applications for Allied Pumps’ industrial water tanks include: fire protection, dust suppression, truck wash, potable water, raw water, wastewater, and industrial liquids.
Yes, Allied Pumps’ industrial water tanks can be customised to be cyclone rated. We have completed many tank projects in regions affected by high wind loads and tropical cyclones.
























































































