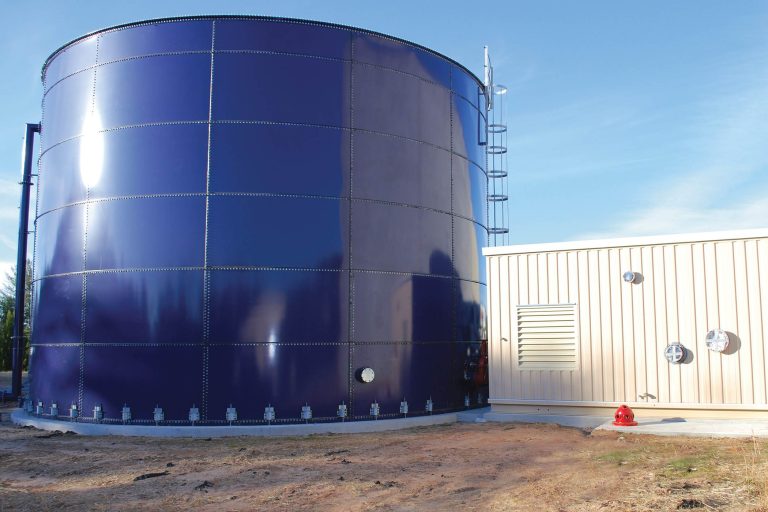
Designed for performance in demanding environments, Allied Pumps’ industrial water tanks provide robust, high-capacity storage for both mines sites and process plants.
Manufactured to rigorous Australian Standards using corrosion-resistant materials, they are built to withstand extreme conditions.
With flexible configurations and capacities, these tanks can integrate efficiently with pumps to provide reliable water supply for potable, process, wastewater, and fire protection.

The tank jacks are equipped to every vertical joint around the tank.


All external fittings and accessories are installed once the tank is at specified height.



Formed in 1905 to obtain, treat and distribute water supplies, the Bunbury Water Board has served the people of Bunbury for over 100 years. The city’s early settlers knew of water stored naturally underground and tried to use it to replace the Collie River and the Preston River, which were the only sources of water for drinking in those days. We supplied the first variable speed system to the water authority. It’s still being used today.

The Cockburn Central Police Station required several tank and pump solutions. Initially a galvanised regular tank was recommended. However, there were design issues with the concrete slab. The station requested an in-situ concrete tank liner. The design was changed to meet this need. Allied Pumps was able to provide a turnkey solution for our client on this project, saving the client from having to engage the services of several different sub-contractors to work on various aspects of the tank installation. This enable the client to place a single order with us for all the work on the tank and supply of the pumping systems, enabling him to focus on other aspects of the project. The final project consisted of a panel tank, circulating pump pack, hot water circulator, fire pump and tank liner pack. The result was a seamless integration between the pumps and the tanks, and reliable fire protection has been the overall outcome.

Blockages occur fairly regularly at Graylands Hospital, Western Australia’s largest mental health facility. Objects and clothing were often being introduced into the plumbing system. With 1,053 fixtures, the system needed help breaking up these foreign objects. Two of their grinder pumps were not properly handling foreign objects. After much investigation, the most practical option was to install a channel grinder in the existing mechanical screening pit. We designed specialised guiderails from 316 stainless steel. They were built in-house to suit the existing concrete structure. This solved the issue and eliminated peak flow blockages. The system has now been up and running for 24 months with no issues.

Located on the Burswood Peninsula, the Optus Stadium is part of a large redevelopment that has become a draw card to thousands of people. However, as with all new developments there was a significant change to the existing landscape. Part of the Optus Stadium is bounded by the Swan River and river traffic, some of the retaining walls and steel piles on the water’s edge which could be seen from the water and needed to be addressed which could not be achieved using a land based planting scheme or additional construction. Allied Pumps created an environmentally sound and sustainable floating treatment wetland that can be configured in rafts of endless configurations. They can fit any existing space or water body shape and can operate in fluctuating water levels which was an essential requirement for this project. While the floating treatment wetlands are primarily a water treatment tool, they have the added bonus of being visually appealing with the use of wetland sedges, rushes and grasses providing fast and easy to install beautification options.

The Perth City Link bus port is reconnecting Northbridge with the city centre, extending from the Perth Station to the new Perth Arena. The bus port required sufficient water storage for protection against fire. Delivering water storage in an underground situation is challenging but necessary. We had several hurdles to overcome. Our ultimate solution was to recommend our dual diesel fire protection pump set. This included suction and discharge manifolds combined with dual rectangular steel liner panel tanks. We manufactured the complete fire pumps skid at our production facility, so they could be tested at our test facility. Installing the tanks onsite was then a challenge in the tight confines of the underground plant room. The successful outcome offered a sufficient amount of water that could be dumped quickly in the case of a sudden fire.

We were recently involved in supplying fire protection for Perth Airport. View the video to see the testing DFES conducted at the facilities in March 2017.

Located on Connelly Street at the Greater Sports Ground is the new built recreation & leisure centre incorporating the Kellerberrin & Districts Club. This was the site of the first concrete pump station in Western Australia. When wastewater has to get to the treatment facility and gravity is not cooperating, precast concrete pump stations do the heavy lifting. Precast concrete pump stations are designed, fabricated and installed with the highest-quality materials and equipment. We installed this system in the early 1990s. Completing a project like shows how we adopt innovation in out techniques.

The National Anzac Centre is one of Australia’s most important cultural pilgrimages. Located within Albany’s heritage listed Princess Royal Fortress, the centre overlooks the actual harbour from which over 41,000 men and woman departed Australia for the Great War. The project required a complete sewage system in a short amount of time. The system needed to handle minimal sewage flow but be prepared for high peak loadings. This is often hard to deliver, but our systems delivered a solution to ensure optimal operation.

The Australian Embassy in Jakarta, Indonesia required a water supply system. Because of its location, this was a very unique project. The spec required the materials to be stainless steel and fibreglass to resist corrosion. The site also needed a controller to monitor and operate water supply valves to fill tanks for use at the building. The three water supplies were the result of rainwater runoff from the roof, bore pumps and mains piping. To ensure that the specs were met, the valves were programmed to operate depending on the supply availability. The competing requirements of this project as well as working in a foreign environment created a number of challenges. We were able to rise to the challenge, through our strong organisational skills and execution of work.

Allied Pumps recently provided 2 Circular Colour Finished Steel Water Storage Tanks to a client near the edge of the water at the Kwinana Bulk Jetty. This area of Cockburn Sound is of significant economic and social importance as it facilitates trade to Western Australia and the nation. It is also subjected to very high winds (almost cyclonic during bad weather events) so special design considerations had to be incorporated into the tank design and construction. The tanks were constructed to 3mm in thickness all over (instead of the normal 3mm on the bottom strake and 1.95mm on the others). The tanks were fitted with harness points on the roof and installed with 2 SWAH doors per tank (normally one). The tanks were also powder coated in colorbond Off White finish to fit in with the surroundings.

A below-water-table mine in East Pilbara required rapid groundwater removal under strict site specs. Allied Pumps engineered six mobile bore headworks systems with telemetry and SCADA integration, enabling efficient dewatering while minimising disruption during active mining.

The remote Pilbara mine required 24/7 dewatering with limited access, high diesel use, and no power for controls. Allied Pumps supplied diesel transfer skids, a 5kL/62kL fuel system, and solar telemetry, enabling SCADA monitoring, lower fuel logistics, and reliable flow control.

Challenged with harsh Pilbara conditions and saline groundwater, the client needed a compliant bore field with SCADA integration. Allied Pumps delivered 24 skid-mounted systems with 316 stainless steel pumps and telemetry, completing installation in 24 weeks and enabling reliable raw water supply.
Allied Pumps’ industrial water tanks are manufactured from panels made of galvanised steel, hot-dip galvanised steel, glass fused steel, and epoxy coated steel.
Sizing for Allied Pumps’ industrial water tanks ranges from 10kL to 30ML. Please reach out to our team if you are looking for other sizes.
Yes, Allied Pumps’ industrial water tanks are designed to meet Australian Standards like AS2304 (Fire Protection) and AS1170 (Wind Loads).
Applications for Allied Pumps’ industrial water tanks include: fire protection, dust suppression, truck wash, potable water, raw water, wastewater, and industrial liquids.
Yes, Allied Pumps’ industrial water tanks can be customised to be cyclone rated. We have completed many tank projects in regions affected by high wind loads and tropical cyclones.
























































































