Built for demanding mining environments, our standpipe systems deliver fast, efficient water transfer from dams, ponds and storage areas to support critical site operations.
Available in sizes from 100mm to 400mm and engineered to withstand cyclone conditions, they ensure reliable performance in harsh environments.
With flexible configurations and durable material options, our standpipes can also be seamlessly integrated with pumps. We aim to provide a practical, cost-effective solution for dust suppression, water cart filling and ongoing site water management.
Challenged with harsh Pilbara conditions and saline groundwater, the client needed a compliant bore field with SCADA integration. Allied Pumps delivered 24 skid-mounted systems with 316 stainless steel pumps and telemetry, completing installation in 24 weeks and enabling reliable raw water supply.

The remote Pilbara mine required 24/7 dewatering with limited access, high diesel use, and no power for controls. Allied Pumps supplied diesel transfer skids, a 5kL/62kL fuel system, and solar telemetry, enabling SCADA monitoring, lower fuel logistics, and reliable flow control.

Faced with tight timelines and complex compliance, the client needed relocatable bore headworks built for 20-year use. Allied Pumps delivered skid-mounted, plug-and-play systems with VSD control and telemetry, enabling remote monitoring and lifting system availability from <80% to near 100%
Allied Pumps’ standpipes are available in heights ranging from 5m to 8.5m, and in diameters ranging from DN100 to D400. In terms of flow rate, our standpipes range from 40L/s up to 250L/s.
Vehicles compatible with Allied Pumps’ standpipes include: CAT 789, CAT 785, CAT 777, and CAT 773 rigid water carts. They are also suitable for smaller rigid/semi water carts.
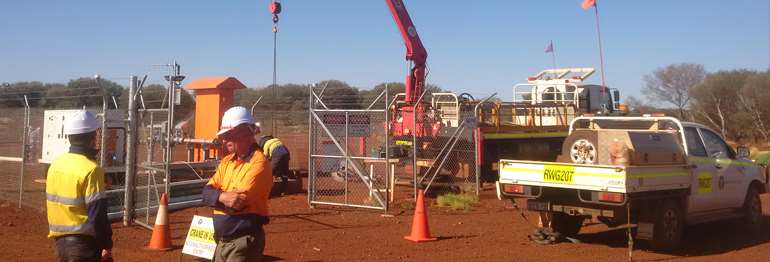
Allied Pumps’ standpipes can be installed without the need of working at heights. A crane can lift the standpipe into place while installers safely secure the structure.
Allied Pumps’ standpipes are engineered & certified to AS/NZS 1170 for Cyclonic Conditions. Additionally, we can provide cyclonic tie downs for Wind Region A to D.
Yes, Allied Pumps provide stop/start controls with remote fob as an add-on option for our standpipes.
























































































